
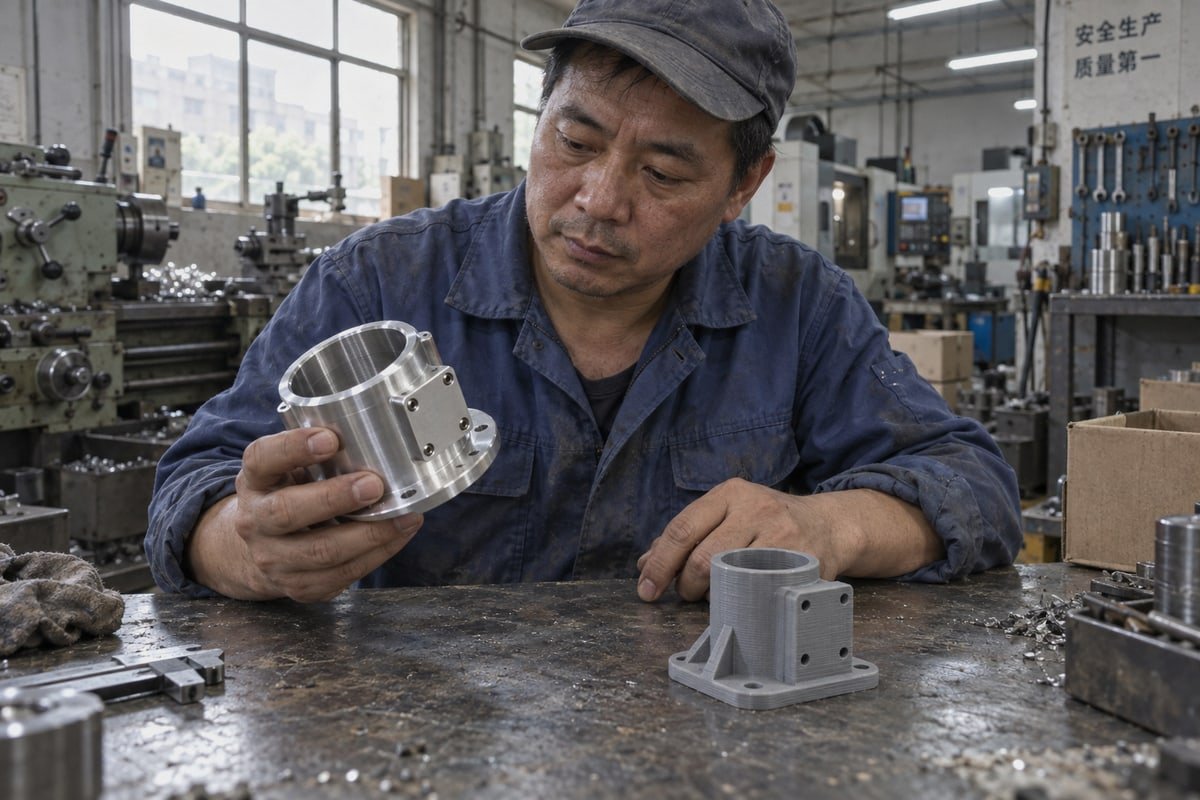
Every week, engineers send our Dongguan workshop the same question: CNC machining vs 3D printing — which one should they trust? Picking wrong wastes budget, delays launches, and kills projects.
Choose CNC machining when you need tight tolerances, strong isotropic material properties, smooth surface finish, and repeatable medium-to-high production volume. Choose 3D printing for rapid prototyping, complex internal geometry, and low-volume customization. Many teams print early prototypes, then switch to CNC for functional and end-use parts.
Neither process is a universal winner. Each one answers a different manufacturing problem. In this guide, I will break down cost, precision, strength, and volume so you can match the right process to your part.
How do I decide between CNC machining and 3D printing for my project?
A German buyer once emailed us two files: a printed bracket and a machined housing. His question was simple — how do we actually decide which process fits which part?
Decide using four variables: part geometry, production volume, mechanical requirements, and lead time. Pick 3D printing for complex shapes, fast iteration, and one-off models. Pick CNC machining for load-bearing parts, tight tolerances, production-grade metals, and repeat batches. Match the process to the part, not the trend.
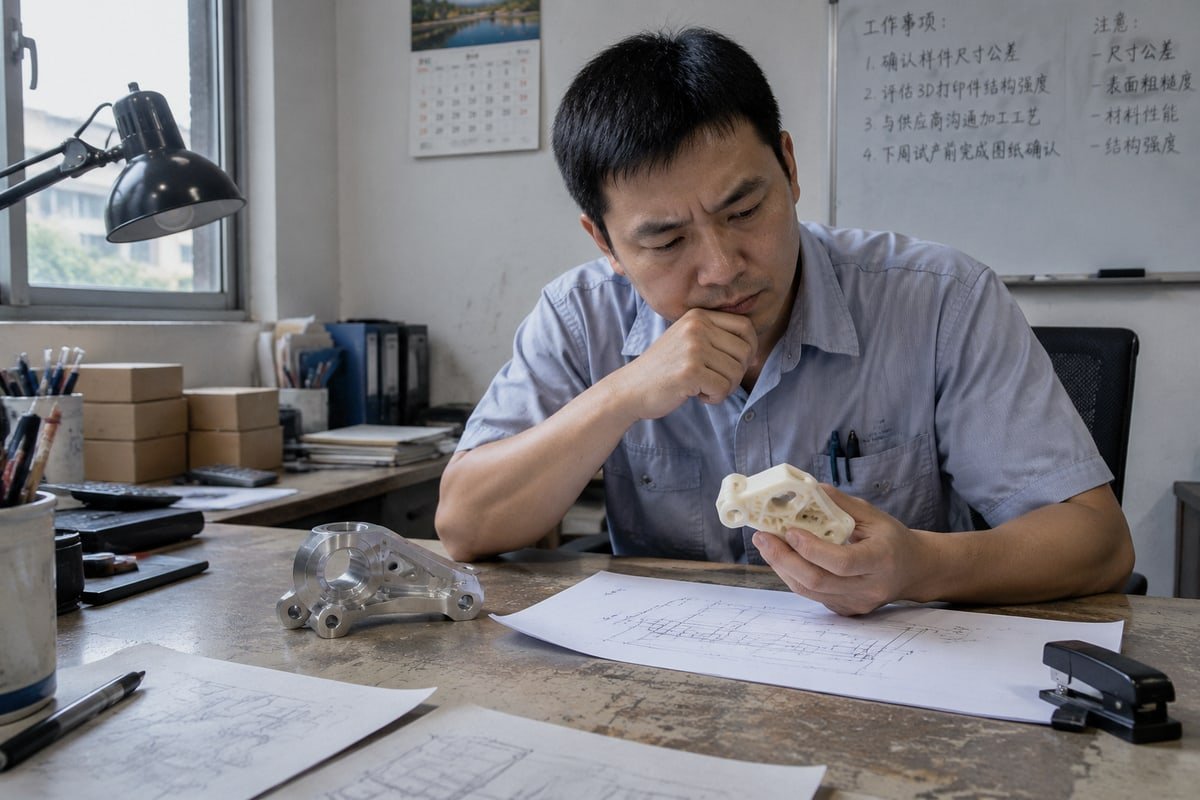
The core difference is direction. CNC machining is subtractive manufacturing. It starts with a solid block and cuts material away with computer-controlled tools. 3D printing is additive manufacturing. It builds the part layer by layer from a digital file. That single difference drives almost every trade-off between them.
The side-by-side comparison
| Criteria | CNC加工 | 3D Printing |
|---|---|---|
| Process type | Subtractive (cuts from stock) | Additive (builds in layers) |
| 寛容 | ±0.005 to ±0.025 mm | ±0.1 to ±0.5 mm |
| Surface finish | Ra 0.8–3.2 µm as-machined | Ra 6–25 µm, needs post-processing |
| Strength | Bulk, isotropic properties | Layer lines can create weak points |
| Materials | Metals, engineering plastics 1, composites | Mostly polymers, growing metal options |
| Complexity | Limited by tool access | Internal channels and lattices possible |
| Best volume | Medium to high batches | One-offs and small runs |
| Material waste | Higher (chips and scrap) | Lower (uses only what the part needs) |
The limitation lens
I always tell buyers to compare limitations first, then advantages. CNC struggles with internal lattices and deep undercuts because the cutter must physically reach every surface. Printing struggles with dimensional accuracy 2, finish, and layer strength. Here is a nuance many people miss: a part that looks complex is often still cheaper to machine. Our 5-axis mills reach compound angles and curved surfaces that seem "unmachinable" at first glance. Geometric complexity only favors printing when tool access is truly impossible. So define your target use case first — concept model, functional test, or end-use part — and the answer usually becomes obvious.
What are the real cost differences between CNC machining and 3D printing?
Last year, we quoted the same aluminum bracket at three quantities for a Canadian client. The results surprised him, and they explain the whole cost story better than any theory.
3D printing usually costs less for one part or very small batches because setup is minimal. CNC machining carries higher programming and fixturing costs upfront, but cost per part drops sharply as quantity rises. At around 50 to 100 parts, CNC often becomes the cheaper option.
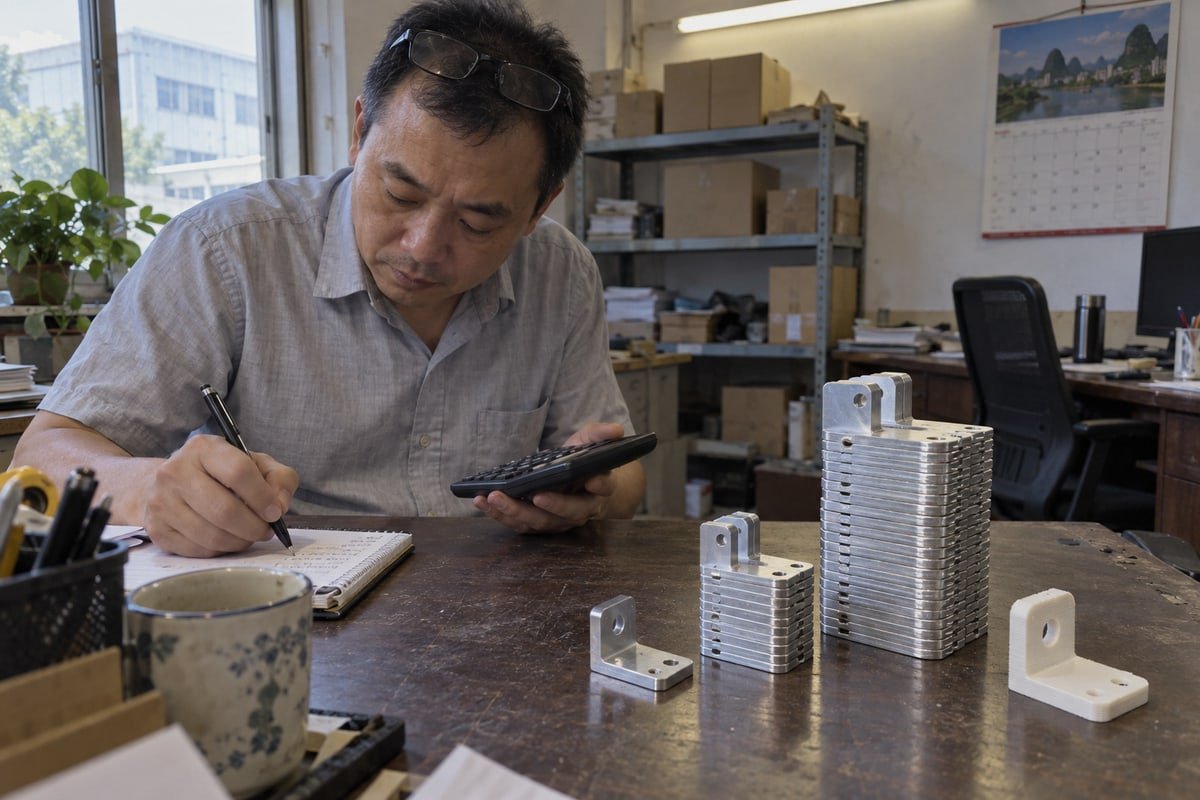
The honest answer to "which is cheaper" is always another question: how many parts do you need? Quantity changes everything.
Cost behavior by volume
| Quantity | 3D Printing | CNC加工 | Likely Winner |
|---|---|---|---|
| 1 piece | Low setup, fast start | Programming and fixturing dominate the price | 3D printing |
| 10 pieces | Still economical | Setup cost spreads out | Depends on geometry |
| 100 pieces | Print capacity becomes a bottleneck | Cycle times drop, unit price falls | CNC machining |
| 1,000+ pieces | Rarely competitive | Fully amortized setup, stable unit cost | CNC machining |
You may have read that CNC can cost five to ten times more than printing. That figure is real in some scenarios — usually a single, complex, one-off part. But it is not a universal rule. Once our machines are programmed and fixtured, the cost per part collapses. At 100 pieces, machining frequently beats printing on both price and speed.
The hidden costs both sides carry
Watch out for costs that never appear in the first quote. Printed parts often need support removal, sanding, and dimensional refinement before they are usable. Machined parts may need custom fixturing for odd shapes. Lead times follow a similar curve: a printed prototype might arrive in 1–3 days versus 3–7 days for a first machined part. But for 100 parts, CNC is often faster overall because printers hit capacity limits. In our experience quoting for European and North American buyers, clear DFM feedback upfront prevents most of these surprises. We flag cost drivers on the drawing before production starts, because an unexpected invoice damages trust more than any delay.
Which process gives me better precision and material strength for my parts?
During a recent CMM inspection at our metrology station, we verified a batch of optical housings to ±0.005 mm. That check is where the precision gap becomes visible, not theoretical.
CNC machining delivers better precision and strength. Machined parts hold tolerances of ±0.005 to ±0.025 mm with Ra 0.8–3.2 µm finishes, and keep the bulk, isotropic properties of solid stock. 3D-printed parts typically hold ±0.1 to ±0.5 mm and can be weaker between layers.
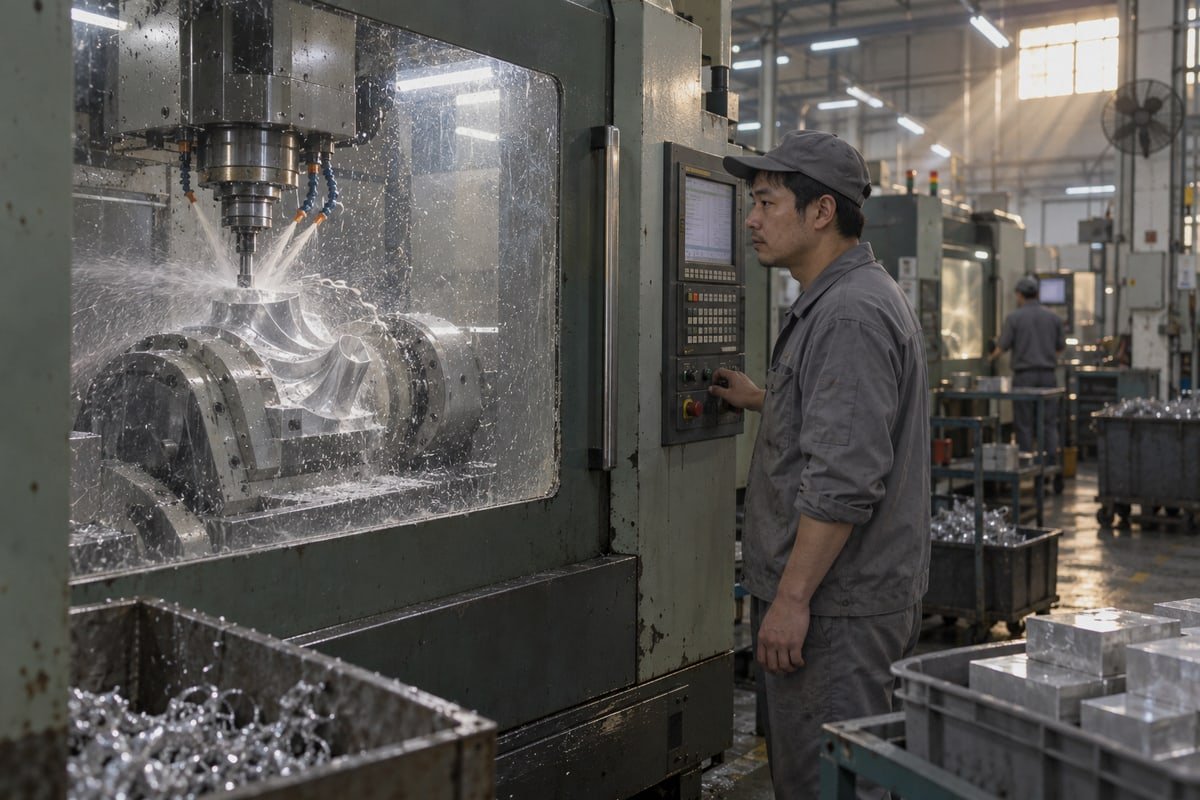
Precision is not one number. It covers dimensional accuracy, surface finish, and consistency across a batch. CNC leads on all three, and the reason goes back to physics.
Why machined parts are stronger
A machined part starts as forged or extruded stock. Its material properties are uniform in every direction — engineers call this isotropic. A printed part is built from fused layers. The bond between layers is usually weaker than the material within a layer. This creates directional weakness, often called Z-axis weakness or anisotropy. For a decorative model, that does not matter. For a load-bearing bracket in an automation machine, it can mean failure. That is why aerospace and medical components still default to machining, where ±0.025 mm tolerances are the working standard.
Precision and materials at a glance
| Factor | CNC加工 | 3D Printing |
|---|---|---|
| Typical tolerance | ±0.005 to ±0.025 mm | ±0.1 to ±0.5 mm |
| Surface finish | Ra 0.8–3.2 µm | Ra 6–25 µm |
| Strength behavior | Isotropic, predictable | Anisotropic, orientation-dependent |
| Material range | Aluminum, stainless steel, titanium, brass, PEEK, POM, nylon | Polymers, resins, select metal powders |
Material availability matters too. On our production floor, we machine aluminum, stainless steel, copper, brass, titanium, and tool steel, plus engineering plastics like PEEK, POM, and PPSU. Printing supports a narrower, process-dependent range. And remember: "printable" does not always mean economically or reliably printable at your required grade. When the drawing specifies 6061-T6 or 316 stainless with a material certificate, machining from certified stock removes all doubt.
Should I choose CNC machining or 3D printing for prototyping versus mass production?
The trade-off I weigh most often for clients is iteration speed against production readiness. A prototype that cannot represent the final part creates false confidence — a lesson several customers learned the hard way.
Use 3D printing for early prototypes and concept models, where speed and design freedom matter most. Use CNC machining for functional prototypes, validation builds, and mass production, where accuracy, material properties, and repeatability matter. Many successful projects print first, then machine for final production.
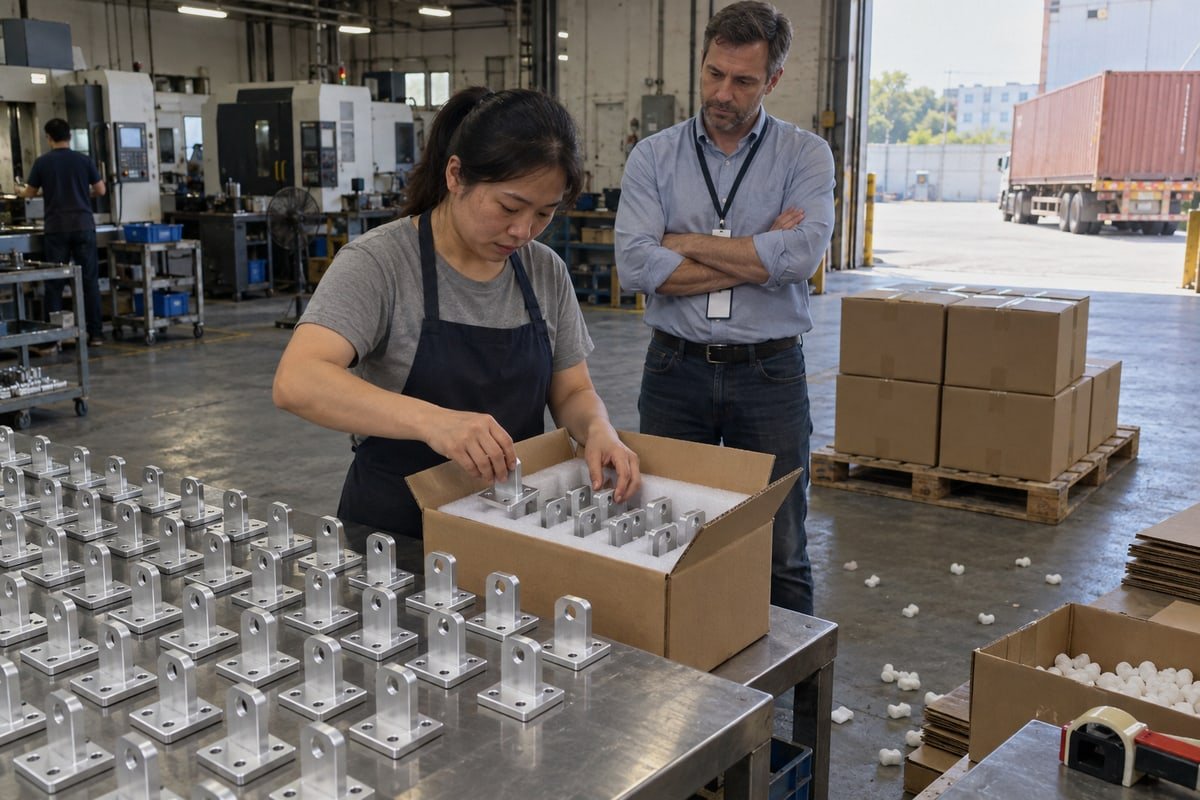
The CNC machining vs 3D printing question changes as your project matures. Early on, you need speed and cheap iteration. Later, you need parts that behave exactly like production parts. Here is the practical sequence I recommend.
A simple decision checklist
- Concept model or fit check? Print it. Speed beats precision at this stage.
- Functional test under real loads? Machine it. You need production material properties, not a look-alike.
- Custom one-off or highly personalized part? Print it, unless it carries load or needs tight fits.
- Batch of 50 to 100+? Machine it. Repeatability and unit cost favor CNC.
- Certified end-use part? Machine it, with inspection reports and material certificates.
Where the two processes now work together
Hybrid manufacturing is the trend worth watching. Some teams print a near-net shape, then finish critical surfaces by CNC to hit final tolerances. Others maintain a digital inventory, printing legacy spare parts on demand instead of warehousing them. AI-driven generative design 3 is also pushing organic, optimized shapes toward printing, since traditional toolpaths cannot replicate them affordably. But be careful with sustainability claims. Printing wastes less raw material, yet total energy consumption per part in high-volume CNC production is frequently lower than long print cycles running for days. At our ISO 9001:2015 4 certified factory, we support this full journey — rapid prototyping in as little as 5 days, then low-volume runs, then mass production on the same drawings with first article inspection. Stable batches, not just good samples, are what get products to market.
Conclusion
CNC machining wins on precision, strength, and scaled production volume. 3D printing wins on speed, geometric complexity, and one-offs. Match the process to your part — or combine both wisely.
Footnotes
1. Technical overview of high-performance polymers used in industrial machining for their superior mechanical and thermal properties. ↩︎
2. NIST resource on metrology and the standards for measuring precision in manufactured components. ↩︎
3. Explains how AI-driven design creates complex geometries often optimized for additive manufacturing processes. ↩︎
4. Official standard for quality management systems, ensuring consistent production quality in manufacturing environments. ↩︎

 日本語
 English
 Italiano
 Français
 Deutsch (Sie)
 Español
 Русский
 العربية
 Български
 Čeština
 Dansk
 Suomi
 עִבְרִית
 हिन्दी
 Nederlands
 Português
 Română
 Slovenčina
 Svenska
 ไทย
 Tiếng Việt
 Türkçe
 Slovenščina