
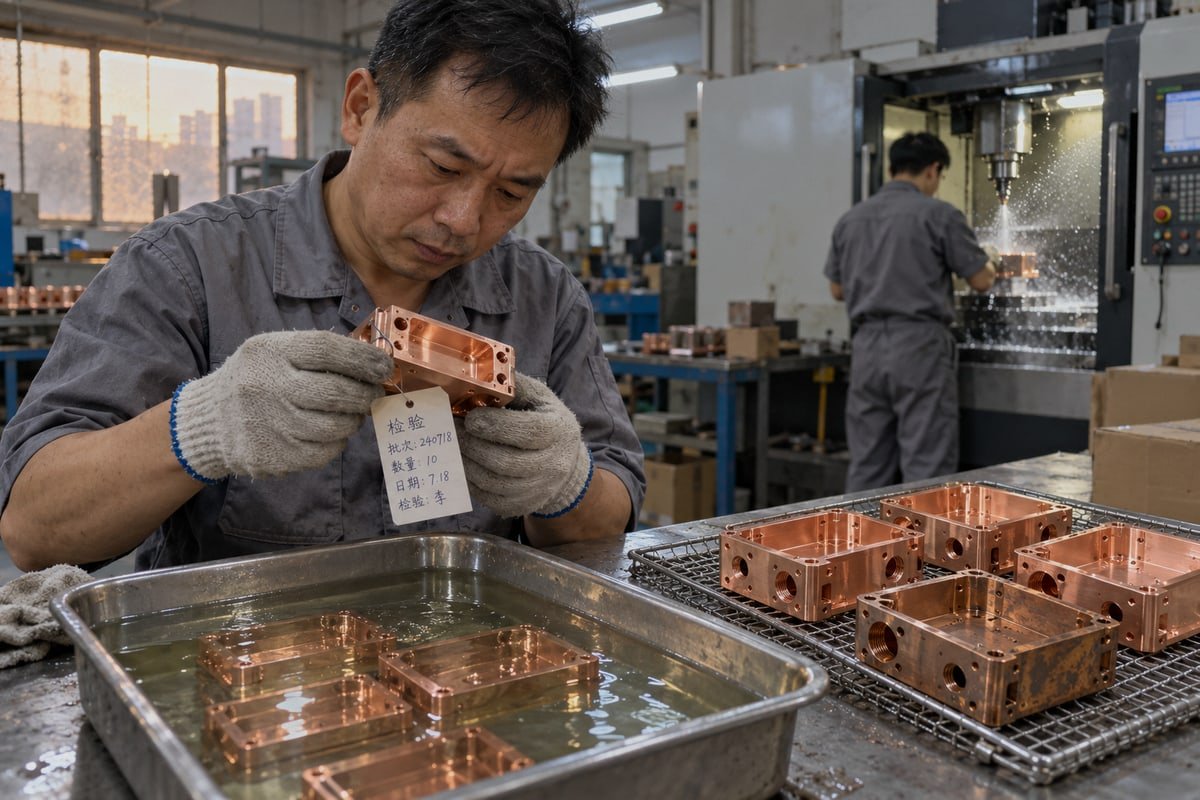
Copper RF housings tarnish fast. One buyer showed us a part that turned brown before assembly because his copper CNC machining service skipped anti-oxidation treatment. The rework cost him weeks.
Choose a copper CNC machining service that machines your exact copper grade regularly, protects parts from oxidation right after cutting, proves tight dimensional tolerances with inspection reports, offers plating and finishing in-house, and quotes the full delivered part with clear lead times.
That is the short answer. The long answer is about evidence. Copper is soft, gummy, and quick to oxidize. It punishes generic shops. Below, I walk through the four areas we check on our own copper line, and the questions I would ask any supplier before placing an order.
What Should I Look for in a Copper CNC Machining Supplier’s Experience and Capabilities?
Our Dongguan shop runs aluminum and brass all day, but copper gets its own tooling drawer. Sharp polished carbide, two-flute end mills, flood coolant. That lesson took years.
Look for regular experience with your exact copper grade, comparable part examples, sharp positive-rake carbide tooling, high-pressure coolant, soft-jaw or vacuum workholding for soft material, multi-axis CNC milling and turning, and written DFM feedback that flags thin walls and deep pockets.
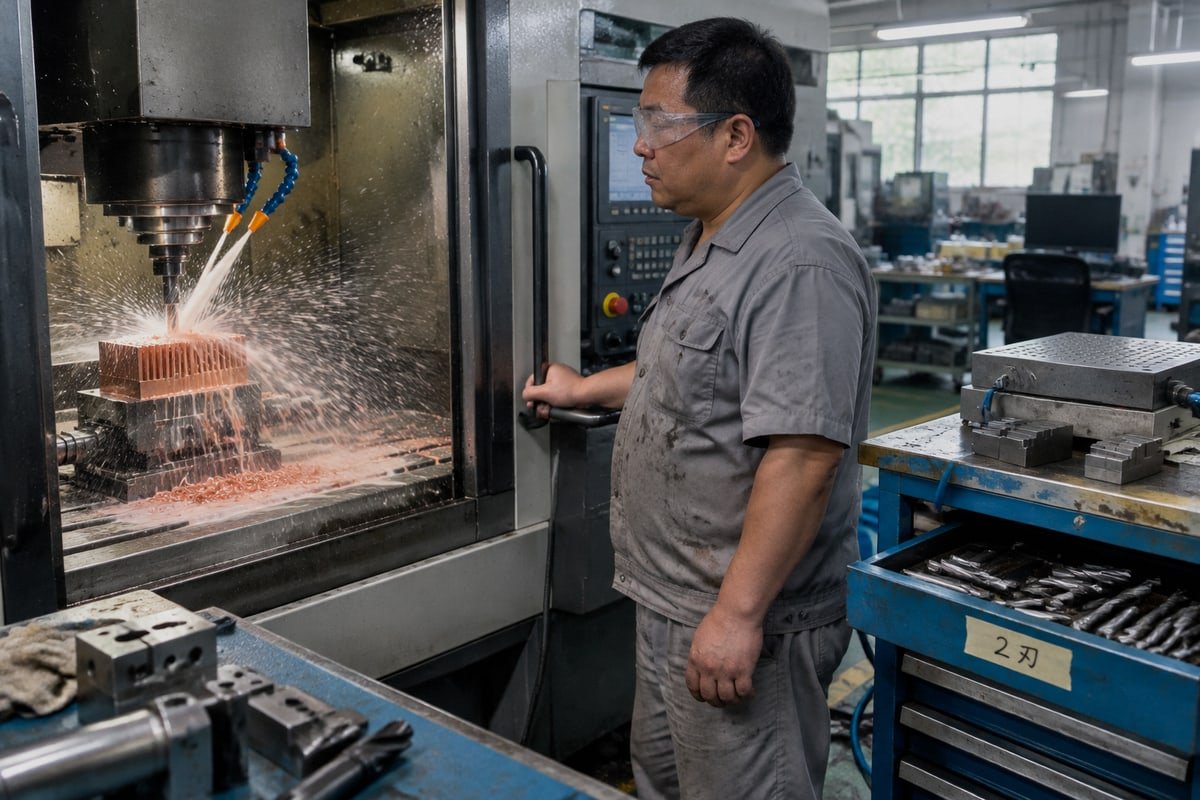
A modern machine list proves very little. We have seen shops with five-axis centers scrap copper electrodes because the chips welded to the cutter. The machine was fine. The process was not. So I start every supplier review with one question: what does copper do differently in your shop?
Why copper needs its own process
Copper behaves unlike steel or aluminum in four ways. It is ductile, so it smears and throws heavy burrs. It pulls heat away from the cut, so the tool edge runs cooler but the chip runs hotter. It sticks to cutting edges and forms built-up edge. And it deforms under clamping pressure. Each of these needs a specific control.
| Copper behavior | What a capable supplier does about it |
|---|---|
| Material adhesion and built-up edge | Sharp, polished carbide or HSS with positive rake; DLC or TiAlN coatings |
| Heavy burr formation | Two-flute tools for chip clearance, defined edge-break, controlled deburring |
| Poor chip evacuation in pockets | High-pressure or continuous flood coolant, DFM review against deep narrow pockets |
| Clamping deformation on thin walls | Soft jaws, custom fixtures, vacuum workholding, balanced material removal |
| Rapid oxidation after cutting | Anti-oxidation treatment or plating scheduled right after machining |
Questions I would ask before quoting
Ask which copper grades the shop runs every week, not once a year. Ask for photos or drawings of similar parts, such as electrodes, heat sinks, RF cavities, or custom copper busbars. Ask whether they understand the gap between pure copper and tellurium copper 1 machinability. Ask if they can read a material certificate 2 and check conductivity. Brass or aluminum experience does not transfer automatically.
What a real DFM review covers
Our engineers return a written DFM note on every copper drawing. It covers minimum wall thickness, deep pockets, internal radii, tool access, datum strategy, setup count, burr-sensitive edges, flatness after machining, and plating allowance. One supplier guide cites about 0.5 mm as a starting point for aesthetic copper walls. Treat that as a floor, not a promise. Actual limits depend on alloy, temper, unsupported length, and fixturing.
For electrodes, we often pair CNC milling with wire EDM for sharp internal corners. For liquid-cooled heat sinks in AI servers and EV power electronics 3, high-aspect-ratio micro-channel milling is now a real differentiator. A copper CNC machining service that can show you this kind of part has already solved the hard problems.
How Can I Verify Tolerance and Quality Control Standards Before Choosing a Supplier?
A German buyer once asked us to hold ±0.01 mm across a long copper busbar face. We pushed back on half the callouts and kept the ones that mattered.
Verify quality by requesting ISO 9001 certification, mill test reports with material traceability, a sample first-article inspection report with actual measurements, CMM and conductivity testing capability, a defined burr limit, calibration records, and a pilot run before mass production.
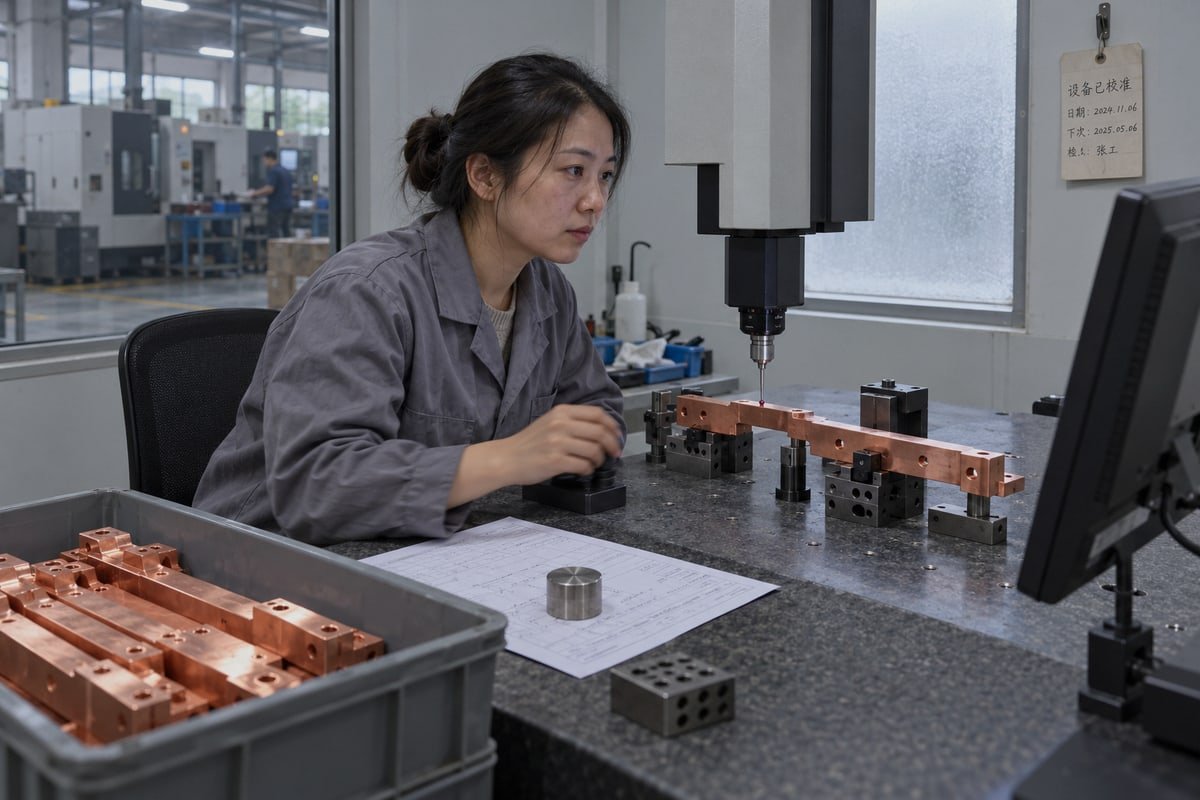
Anyone can write "±0.01 mm" on a website. Our own milling page lists 0.01–0.005 mm, and I know exactly what it takes to hold that in copper. It is not a claim. It is a fixture, a measurement plan, and a temperature-controlled room. So when I evaluate a supplier, I look for measurement evidence, not capability statements.
A simple verification sequence
- Ask for the quality certificate. ISO 9001:2015 is the baseline. AS9100 matters only if your end market demands it.
- Request a sample first-article inspection report from a previous copper job. Look for actual readings, not just "pass."
- Ask how incoming material is verified. A mill test report should show the alloy, temper, and chemistry. Material traceability from bar to finished part should be documented.
- Ask what they measure beyond dimensions. For electrical parts, conductivity. For heat sinks, flatness and parallelism. For electrodes, internal soundness and surface quality.
- Run a small pilot batch before committing to volume. Prototype success does not prove production repeatability.
Evidence versus claims
| Supplier claim | Evidence to request |
|---|---|
| "We hold tight dimensional tolerances" | FAI report with CMM data on a comparable copper part |
| "We use certified material" | Mill test report plus traceability record per batch |
| "Parts are inspected" | Written inspection plan: in-process checks, final checks, sampling level |
| "We deburr all parts" | Maximum burr size, edge-break spec, method, and inspection step |
| "Conductivity meets spec" | Conductivity test method and sample result |
Splitting tolerances by function
Tight tolerances on every dimension raise cost and scrap without improving the part. We ask buyers to sort callouts into critical functional, assembly, reference, cosmetic, and general. Large flat contact faces, thin walls, deep pockets, and multi-setup features are the hardest to hold in soft copper. A good supplier will challenge unnecessary tolerances instead of accepting every number silently.
Burrs are a functional spec
For electrical, RF, and sealing parts, burrs cause real failures: poor contact, damaged insulation, short circuits. "Deburr all edges" is not enough for production control. Mark critical faces on the drawing. Define the limit. Ask how it is inspected. We back our own parts with a 30-day warranty, and burr control is a big part of why we can.
What Copper Grades and Surface Finishes Should I Consider for My Project?
The hardest lesson our copper line taught us is that oxidation starts the moment chips stop flying. We now move finished parts to anti-oxidation treatment the same day.
Use C110 for general electrical and thermal parts, oxygen-free C101 or C102 when conductivity is critical, C145 tellurium copper for machinability, and C18150 or C18200 for strength. Then specify tin, nickel, silver, or anti-oxidation coating before machining to protect the surface.
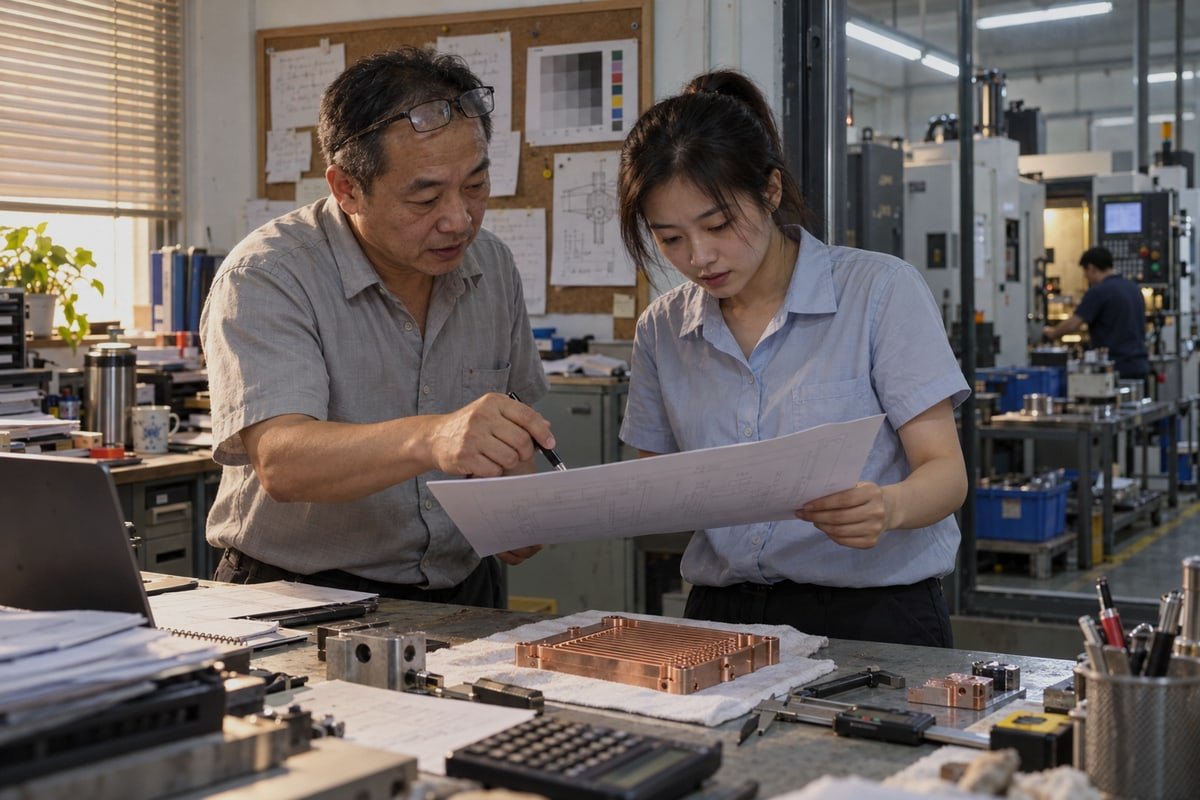
The drawing should never just say "copper." It should name a grade and a temper. The right grade depends on what the part does, not on which copper is purest. Here is how I frame the choice for buyers.
Choosing the grade by function
| Grade | Strengths | Trade-offs | Typical use |
|---|---|---|---|
| C110 (ETP) | Good electrical and thermal conductivity, widely available | Gummy to machine, moderate strength | Busbars, terminals, heat sinks |
| C101 / C102 (OFHC) | Highest purity, oxygen-free copper 4 grades for conductivity and vacuum use | Hardest to machine, costlier | RF cavities, vacuum electrodes, waveguides |
| C145 (tellurium copper) | Tellurium copper machinability is far better, good conductivity | Slight purity loss | Connectors, high-volume turned parts |
| C18150 / C18200 (CuCr, CuCrZr) | Higher strength, hardness, wear resistance | Roughly 10–20% lower conductivity than pure copper | Welding electrodes, mold inserts |
| Beryllium copper 5 | Spring properties, very high strength | Hazardous dust; needs strict safety controls | Springs, contacts |
A common buyer objection is "just use pure copper for maximum performance." I resolve it this way: if the part is an EDM electrode or a resistance-welding tip, pure copper wears out fast. A CuCr grade gives a better total solution even with the conductivity loss. Maximum electrical and thermal conductivity is only the right target when nothing else competes with it.
If beryllium copper is on the table, confirm the supplier has dust extraction, housekeeping, and waste handling procedures. This is a safety issue, not a quality preference.
Surface finishing options and oxidation control
Copper tarnishes within days in humid air. For electrodes, heat sinks, and RF parts, surface quality is part of the function. So finish selection belongs in the design stage.
| Finish | Purpose | Watch out for |
|---|---|---|
| Anti-oxidation treatment | Short-term protection, keeps solderability | Not a long-term barrier |
| Tin plating | Solderability, corrosion resistance | Adds thickness; affects fit |
| Nickel plating | Wear and corrosion barrier | Raises contact resistance |
| Silver plating | Best conductivity at contact surfaces | Cost; tarnish on its own over time |
| Pulido | RF surface quality, appearance | Must not round critical edges |
Another objection: "plating fixes copper's surface problems." Plating changes dimensions, contact resistance, thermal behavior, and fit. It must be designed in, with a plating allowance on the drawing. If a copper CNC machining service adds plating after the fact without that allowance, your bores and threads will be wrong.
How Do I Compare Pricing, Lead Times, and Communication When Selecting a Machining Partner?
Two quotes landed on a US buyer's desk. Ours was higher. The cheaper one excluded inspection, plating allowance, and material certs. He chose us after reading the fine print.
Compare total delivered cost, not unit price. Check what each quote includes: material certs, inspection, deburring, plating, packaging, and shipping. Confirm realistic lead times against capacity, and judge communication by whether the supplier questions your drawing before quoting.
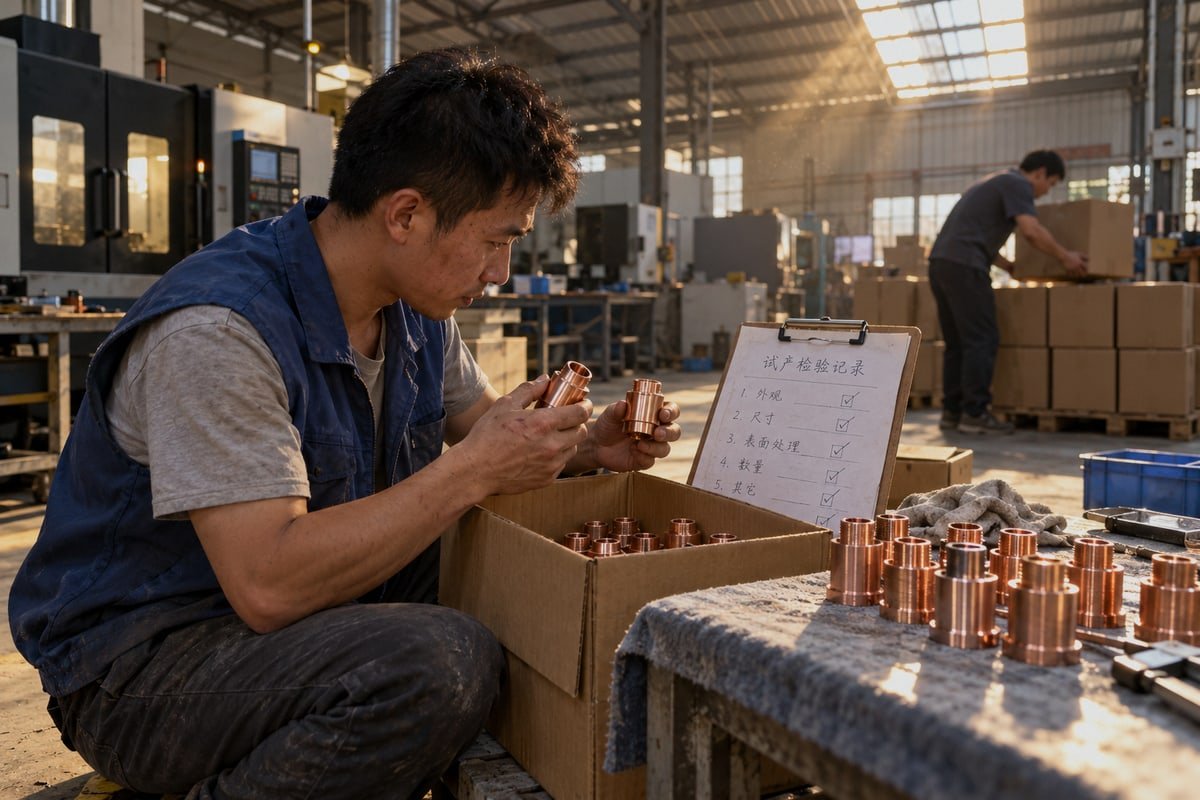
Price is the last thing I look at, and I say that running a shop that competes on "German Quality, Asia Price." The reason is simple. A low copper quote that skips finishing or inspection becomes an expensive quote once the parts tarnish or fail contact tests.
Build a total-cost view
| Cost item | Often hidden in a low quote? |
|---|---|
| Raw material and yield | Yes, if the wrong or cheaper grade is assumed |
| Programming and fixtures | Yes, billed later as "tooling" |
| Deburring and edge-break | Yes, or done to no defined standard |
| Plating or anti-oxidation | Yes, frequently excluded |
| Inspection reports and FAI | Yes, offered only on request at extra cost |
| Packaging for clean, scratch-free parts | Yes |
| Rework and rejection risk | Never shown, always real |
Ask each supplier to state what the price includes line by line. A quote that lists these items is already telling you how the shop thinks.
Read lead times against capacity
Our homepage states lead times as short as 5 days, and we hit that on rapid prototyping services with clear drawings. But I will not promise 5 days on a plated oxygen-free copper production batch. If a supplier gives a very short lead time with no explanation of machine availability, material stock, or plating subcontractor schedule, be careful. Ask whether the prototype will use the same material source, machining route, and inspection plan as production. If not, the prototype proves little.
Judge communication before you order
Good communication shows up in the first reply. Does the supplier ask for the 2D drawing and 3D model? Do they notice a missing alloy or conductivity spec? Do they question a tolerance that conflicts with a plating callout? Our buyers in Germany, the US, and the UK tell us the same thing: an engineer who reads the drawing saves more money than a salesperson who answers fast.
A weighted scorecard
For a high-current connector or RF component, I would weight copper-specific experience around 20%, material control and certification 15%, machining and tooling capability 15%, inspection and testing 15%, tolerance and burr control 10%, lead time 10%, communication and DFM 10%, and total cost 5%. Shift the weights for a decorative part. The point is that cost sits at the bottom, not the top.
Red flags
Walk away if the supplier quotes without confirming the copper grade, treats copper like aluminum, cannot describe burr control, cannot provide material certificates, or answers engineering questions with commercial replies only.
Conclusion
Copper punishes shortcuts with burrs, tarnish, and drift. Pick the service that controls the whole part, not just the cut. Send us your drawing and grade for a technical review.
Footnotes
1. The Copper Development Association provides technical resources and standards for various copper alloys and grades. ↩︎
2. ISO 9001 is the global standard for quality management systems and material documentation in manufacturing. ↩︎
3. The IEA tracks global trends in electric vehicle technology and power electronics infrastructure. ↩︎
4. Wikipedia provides a technical overview of oxygen-free copper grades used in high-conductivity applications. ↩︎
5. OSHA provides safety guidelines for handling beryllium copper due to its hazardous nature. ↩︎

 Español
 English
 Italiano
 Français
 日本語
 Deutsch (Sie)
 Русский
 العربية
 Български
 Čeština
 Dansk
 Suomi
 עִבְרִית
 हिन्दी
 Nederlands
 Português
 Română
 Slovenčina
 Svenska
 ไทย
 Tiếng Việt
 Türkçe
 Slovenščina