
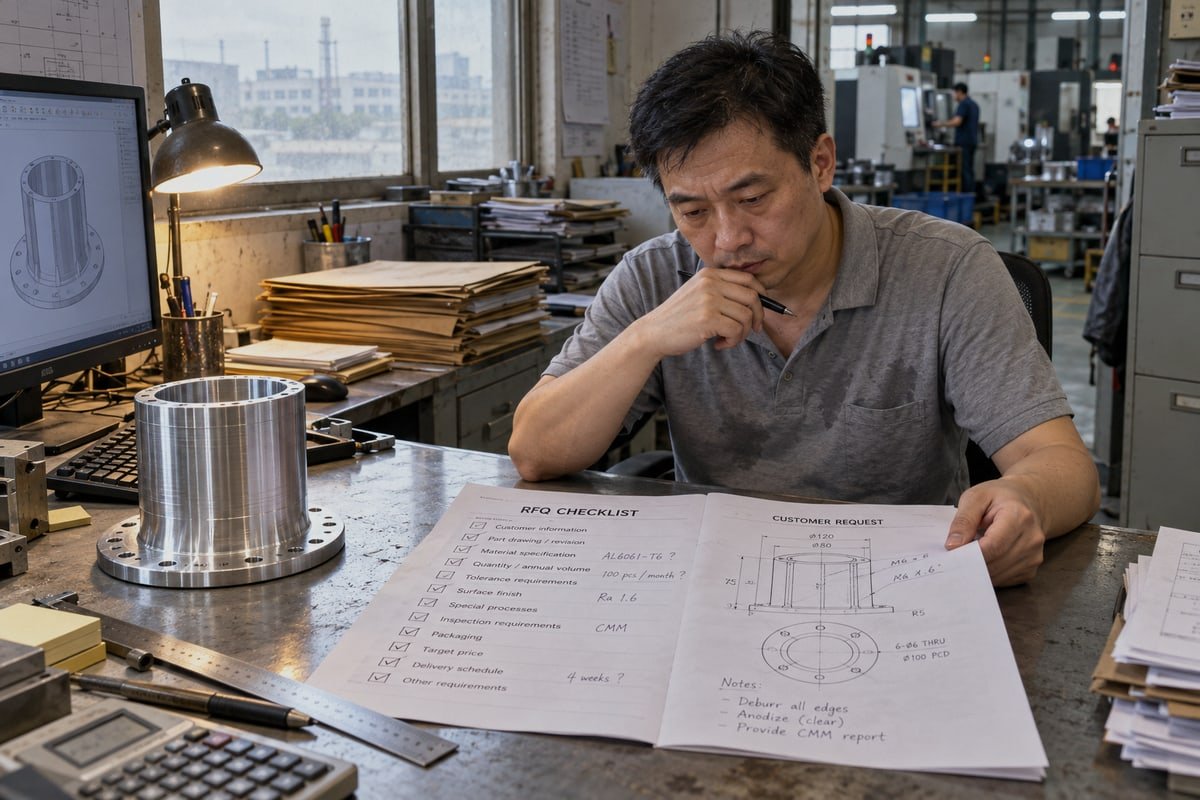
Many RFQs that reach our Dongguan engineering desk lack something basic. Without full information for a CNC machining quotation, you wait, we guess, and prices shift later.
A CNC machining quotation requires a 3D CAD model, a matching 2D drawing with tolerances and GD&T, exact material grade and condition, order quantity, surface finish and post-processing needs, inspection and certification requirements, plus delivery date and destination.
That list looks long. In practice, it answers five questions: what the part is, what it is made from, how many you need, how precise and finished it must be, and when and where it must arrive. Our quoting team prices more than machine time. We estimate programming, setup, fixturing, tooling, inspection, finishing, packaging, shipping, and scrap risk. Each missing input forces an assumption. The sections below show what to send so our quote is firm, not provisional.
What Drawing Details Do I Need to Include for an Accurate CNC Quote?
Last spring a housing STEP file 1 arrived with no drawing. Our programmer built toolpaths in an hour, then stalled for days waiting on thread specs and datums.
Include a current 3D CAD model in STEP or IGES format plus a revision-controlled 2D PDF drawing showing dimensions, tolerances, GD&T datums, thread details, surface finish symbols, material notes, part number, revision level, units, and any critical-to-quality features.
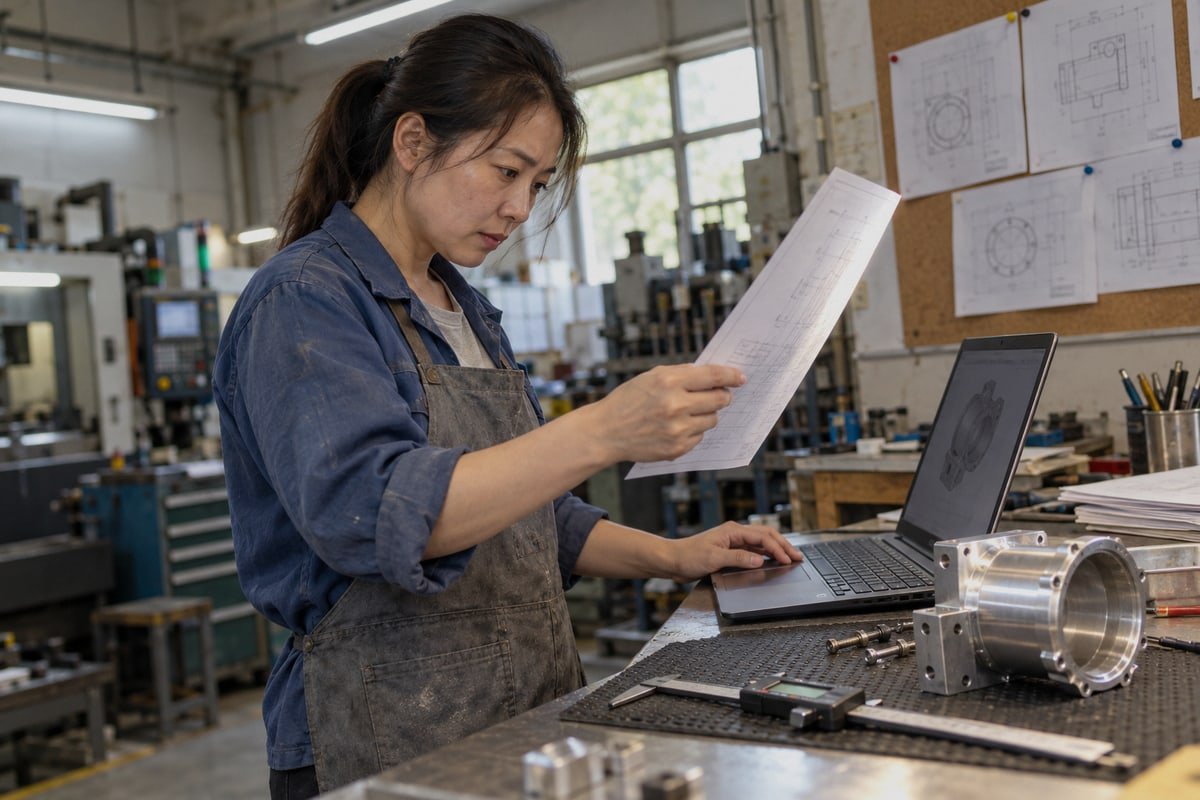
The 3D model and the 2D drawing do different jobs. Our engineers use the model to see geometry. They use the drawing to understand requirements. You need both, and they must agree.
Why a STEP File Is Not Enough
Some buyers push back here. They say online quoting tools accept a single CAD file, so a drawing is optional. That is partly true. A STEP file lets us calculate rough cycle time, check tool access, and spot deep cavities or thin walls. It tells us whether the part needs 3-axis, 4-axis, or 5-axis work. But the model only shows nominal shape. It does not say which bore must hold 0.01 mm. It does not say whether a hole is tapped M6 or drilled for a press-fit insert. So an automated price from a model alone is a preliminary estimate. The drawing turns it into a real CNC machining quotation.
| Item | 3D CAD Model | 2D Technical Drawing |
|---|---|---|
| Nominal geometry | Yes, fully defined | Reference only |
| Dimensional tolerances | Rarely included | Required |
| GD&T standards 2 and datums | Usually missing | Required |
| Thread class and depth | Often ambiguous | Required |
| Surface finish requirements | Not shown | Symbols or Ra values |
| Governing document | Supports manufacturing | Controls inspection and acceptance |
Thread and Tapping Details
Threads cause more clarification emails than any other feature. On the cylindrical housing we machined for an optical customer, the drawing listed the thread callout but not the usable depth. We asked. The answer changed the tap we used and the cycle time. Please state internal or external thread, metric or imperial standard, pitch, class or fit, blind or through, usable thread depth, and any insert or plug-gauge requirement.
A Quick File Consistency Check
Before you send, verify these points:
- The CAD file and drawing carry the same part number and revision.
- Units match across both files.
- The drawing does not reference obsolete geometry.
- Assemblies are sent as separate files per component.
- Filenames include part number, revision, and file type.
If the two documents conflict, tell us which one governs. Mismatched files are a hidden commercial risk. We may price one version while you expect another.
How Do I Specify Materials and Tolerances When Requesting a CNC Machining Quote?
A German buyer once wrote only "stainless steel" on his RFQ. We asked 304 or 316L, and his answer changed the unit price noticeably.
State the exact grade, temper, and raw-material form, such as 6061-T6 aluminum bar, plus any approved substitutes and certification needs. For tolerances, give a general tolerance block, then call out tight tolerances, GD&T controls, and datums only on critical features.
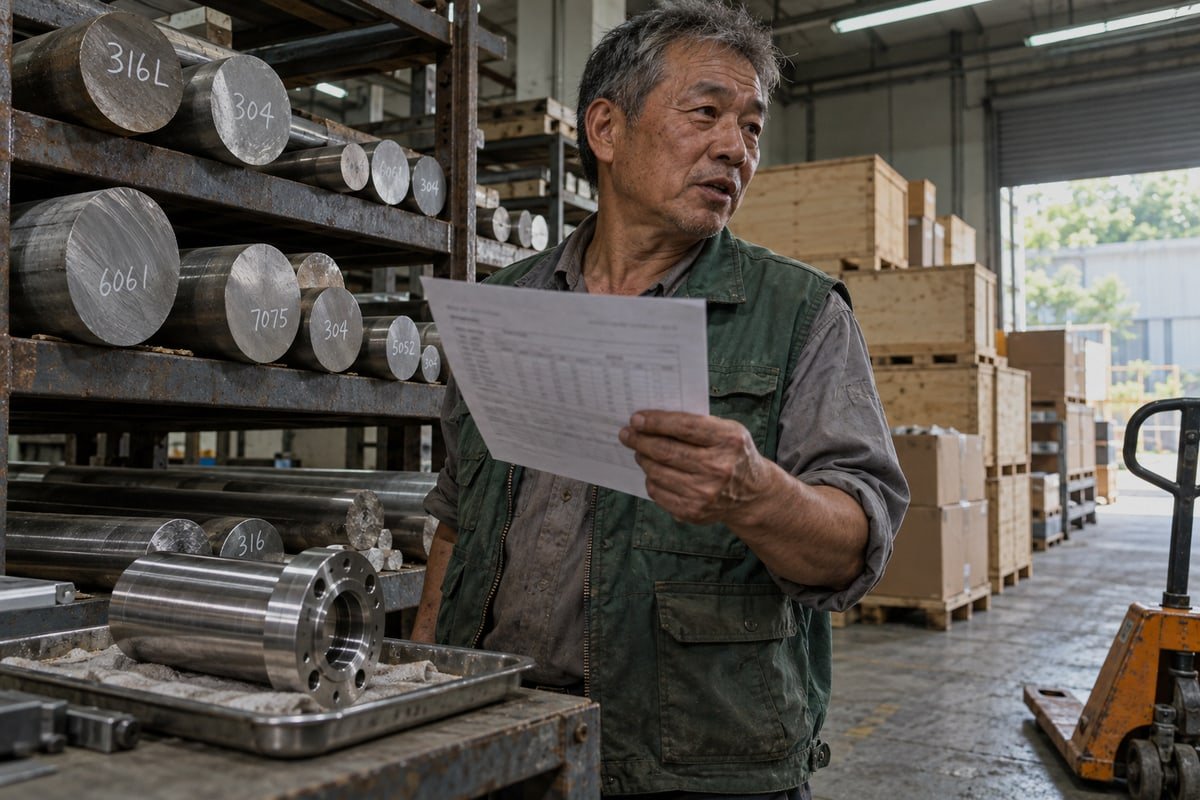
Material and tolerance are the two inputs that swing our price the most. Both reward precision in the RFQ. Both punish vague wording.
Writing Material Specifications That Price Correctly
Generic names hide real cost differences. "Aluminum" could mean 6061-T6 bar or 7075-T6 plate. The two differ in raw cost, machinability, and stock sizes. "Steel" could mean 4140 pre-hardened or a soft mild grade. Our shop machines aluminum, stainless steel, copper, brass, titanium, alloy steel, tool steel, and engineering plastics like PEEK, POM, PPSU, and HDPE. Each one changes cutting parameters, tool wear, and distortion risk. For the mold base shown in our gallery, the customer specified a pre-hardened steel plate with a hardness range. That single line told us the material cost, the tooling we needed, and whether heat treatment came before or after finish machining.
| Material Detail | Example | Why It Changes the Quote |
|---|---|---|
| Grade | 316L stainless steel | Raw cost and machinability |
| Temper or condition | T6, pre-hardened, annealed | Cutting speeds and tool life |
| Raw form | Bar, plate, tube, casting | Stock availability and material waste |
| Hardness or heat treatment | 28–32 HRC after machining | Sequence of operations and distortion |
| Material certifications | Mill test report, traceability | Sourcing restrictions and paperwork |
| Approved substitutes | 6082-T6 acceptable for 6061-T6 | Cost or lead time flexibility |
Some buyers worry that naming an exact grade removes savings. Others worry that allowing substitutes invites material fraud. Our view is simple. Name the exact grade. Then list approved alternatives in writing if you have any. We never substitute without written approval, and we supply material certifications when the RFQ requests them.
Tolerance Requirements: Selective Precision
Our 5-axis cells 3 hold 0.01 mm to 0.005 mm on critical features. We can quote that. But applying it to every dimension on a bracket makes no sense. Tight tolerance requirements mean slower feeds, extra operations, temperature control, more frequent inspection, and sometimes grinding. A buyer once argued for one broad, loose tolerance across the whole drawing to keep things simple. The problem is that suppliers interpret broad blocks differently and price in risk. The clearer approach is a general tolerance block plus explicit GD&T standards on the features that matter: position, flatness, perpendicularity, profile, and the datum structure that ties them together. Mark critical-to-quality dimensions. We will protect those and run the rest efficiently.
What Information About Quantity and Lead Time Should I Provide for My CNC Project?
Every week we weigh soft jaws against a dedicated fixture. The answer depends on one number the RFQ often omits: expected annual demand.
Provide the quantity to quote, prototype and first production quantities, expected annual demand, requested quantity breaks such as 10, 50, 500, and 5,000 pieces, whether orders recur, a firm target delivery date rather than "ASAP", and the destination country for shipping.
Quantity decides how we spread setup and programming cost. Lead time decides which machines, shifts, and shipping options we plan around. Both belong in the RFQ, not in a follow-up call.
Why Order Quantities Change the Strategy
A single prototype and a 500-piece run of the same part are two different manufacturing problems. For one piece, we use flexible methods: standard vises, soft jaws, and a program written for speed, not optimization. For production, dedicated workholding and a tuned process pay back quickly. That is why we ask for tiered pricing requests rather than a single unit price. The tiers show you how setup cost is allocated and where economies of scale begin.
| Quantity Tier | Typical Approach in Our Shop | What You Learn From the Price |
|---|---|---|
| 1–10 prototypes | Soft jaws, general programming, manual inspection | How much setup dominates the unit cost |
| 50–200 pieces | Semi-dedicated fixtures, process checks | Where unit price starts to fall |
| 500+ pieces | Dedicated fixtures, optimized toolpaths, sampling plan | Stable long-run cost for planning |
| Annual blanket | Fixture investment, material reservation | Best price plus delivery scheduling |
Tell us whether the order is one-time or recurring. If you expect to reorder, we build fixtures and keep programs and inspection records on file. That stabilizes dimensions from the first sample through batch production, which is the exact pain point many buyers raise with us.
Setting Lead Time Expectations
"ASAP" gives us nothing to plan with. A specific date does. With a firm date, we can judge capacity, decide whether outside processing fits the window, and choose air or sea freight. Our standard lead times run as short as 5 days for simple parts, but anodizing, heat treatment, or a full inspection report adds days. If your date is flexible, say so. Flexibility often lowers cost. If your date is fixed, say that too, and we will quote expedited capacity honestly rather than promise and slip.
Delivery and Packaging Details
Destination affects duties, taxes, export documents, and packaging. Our customers in the United States, Germany, France, and Japan each have different import routines. Also tell us about packaging: individual wrapping, protective caps, moisture protection, labels or barcodes, and partial shipments. If parts feed an automated assembly line, specify the orientation and tray layout the robotic pick-and-place system expects. A precision part scratched in transit is a failed part, so this detail is worth two lines on the RFQ.
Do I Need to Mention Surface Finishing and Inspection Requirements When Requesting a Quote?
Hard anodizing taught us a costly lesson years ago. The coating thickened a bore past its fit limit because nobody flagged masking on the RFQ.
Yes. Specify Ra roughness values, cosmetic standards, and every post-processing treatment such as anodizing, plating, passivation, or heat treatment, including thickness, color, and masked areas. Also state inspection needs: FAI, CMM reports, material certifications, certificates of conformance, and traceability.
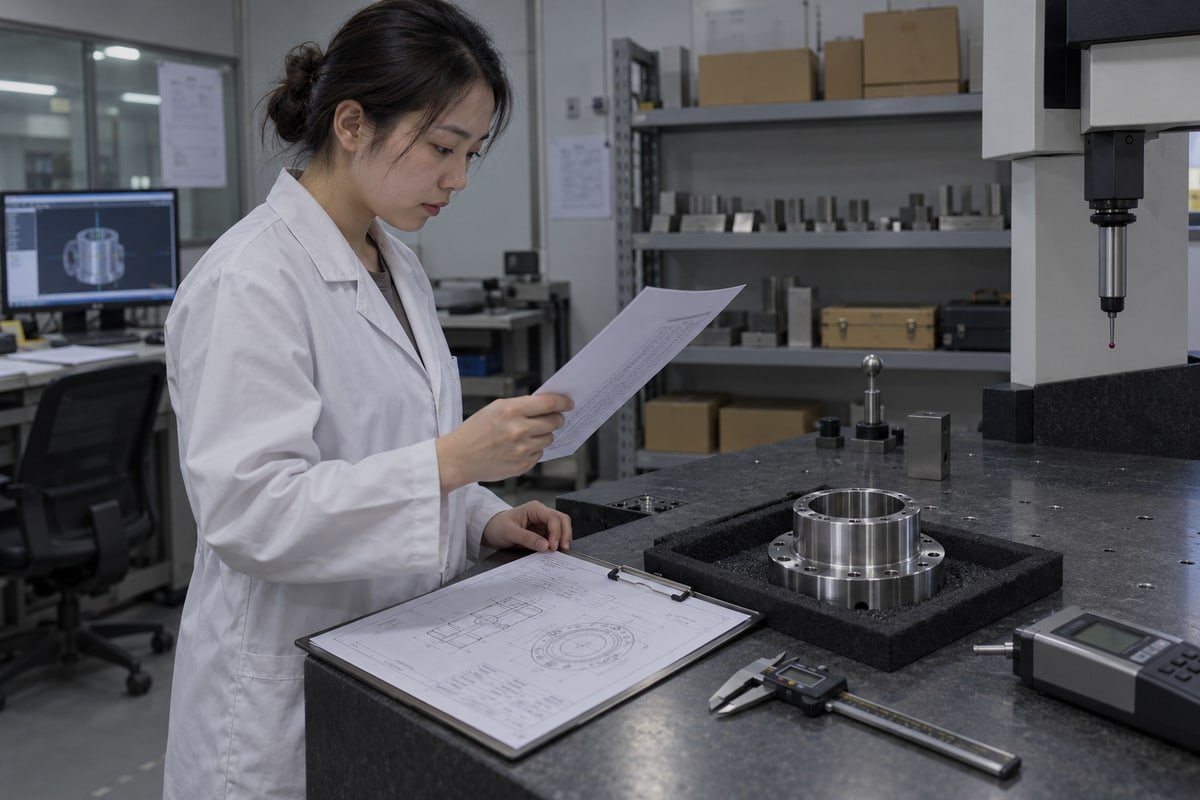
"CNC machined and finished" is not a specification. Neither is "good quality." Both phrases leave the supplier to decide what you receive. Finishing and inspection should be defined before the quote, not added after the purchase order.
Surface Finish Requirements Versus Cosmetic Standards
Two things get mixed up here. One is a machined roughness value, such as Ra 1.6 or Ra 0.8, measured on the surface. The other is a cosmetic or coating requirement, such as bead blast plus black anodize with no visible tool marks on the front face. Say which surfaces each requirement applies to. State lay direction if it matters. Define acceptable scratch or dent limits and the lighting conditions for visual inspection. Our surface finishing department handles anodizing, bead blasting, polishing, passivation, black oxide, and plating, but each one needs a standard, a thickness or color target, and a masking map.
Post-Processing Treatments That Move Dimensions
Coatings add thickness. Heat treatment can distort. Both affect fits and hole sizes. Tell us whether drawing dimensions apply before or after coating. For the housing with the bolted mounting bracket, the customer required the bracket interface to stay bare for conductivity. That note on the RFQ decided our masking plan and the price.
Inspection Required Versus Inspection Report Required
We inspect every part under our ISO 9001:2015 4 system. A report is a separate deliverable. The distinction matters for pricing and lead time.
| Inspection Level | What We Deliver | Typical Use |
|---|---|---|
| Standard dimensional check | Internal records, visual and gauge checks | General industrial parts |
| Inspection report with values | Measured dimensions on critical features | Automation and equipment components |
| First Article Inspection | Full dimensional report on first sample | New part introduction, pre-production approval |
| CMM report plus certificates | CMM data, material test report, coating and heat-treat certificates, certificate of conformance | Medical, aerospace, and optical projects |
Match documentation to real risk. A full traceability package costs more than a sample report, and it should be requested when the application justifies it. If you need RoHS or REACH declarations 5, lot control, or calibration records, list them. If your drawings are export-controlled or covered by an NDA, tell us the data-handling rules up front so we can confirm compliance before quoting. Some corporate buyers now also ask for sustainability or carbon reporting; we can discuss what is practical, but it must be in the RFQ. We back shipped parts with a 30-day warranty, and clear inspection terms make any claim fast to resolve.
Conclusion
Give us the part, the material, the quantity, the precision and finish, and the delivery details. A complete RFQ means a faster, firmer CNC machining quotation with no surprises.
Footnotes
1. Wikipedia entry for the ISO 10303 standard, commonly known as the STEP file format. ↩︎
2. Official site for ASME standards, including the Y14.5 standard for geometric dimensioning and tolerancing. ↩︎
3. Overview of multi-axis CNC machining configurations and their industrial applications. ↩︎
4. Official ISO page for the quality management standard mentioned in the article. ↩︎
5. Updated official European Commission landing page for the RoHS Directive; the previous URL under the chemicals path now returns a 404. ↩︎

 עִבְרִית
 English
 Italiano
 Français
 日本語
 Deutsch (Sie)
 Español
 Русский
 العربية
 Български
 Čeština
 Dansk
 Suomi
 हिन्दी
 Nederlands
 Português
 Română
 Slovenčina
 Svenska
 ไทย
 Tiếng Việt
 Türkçe
 Slovenščina