
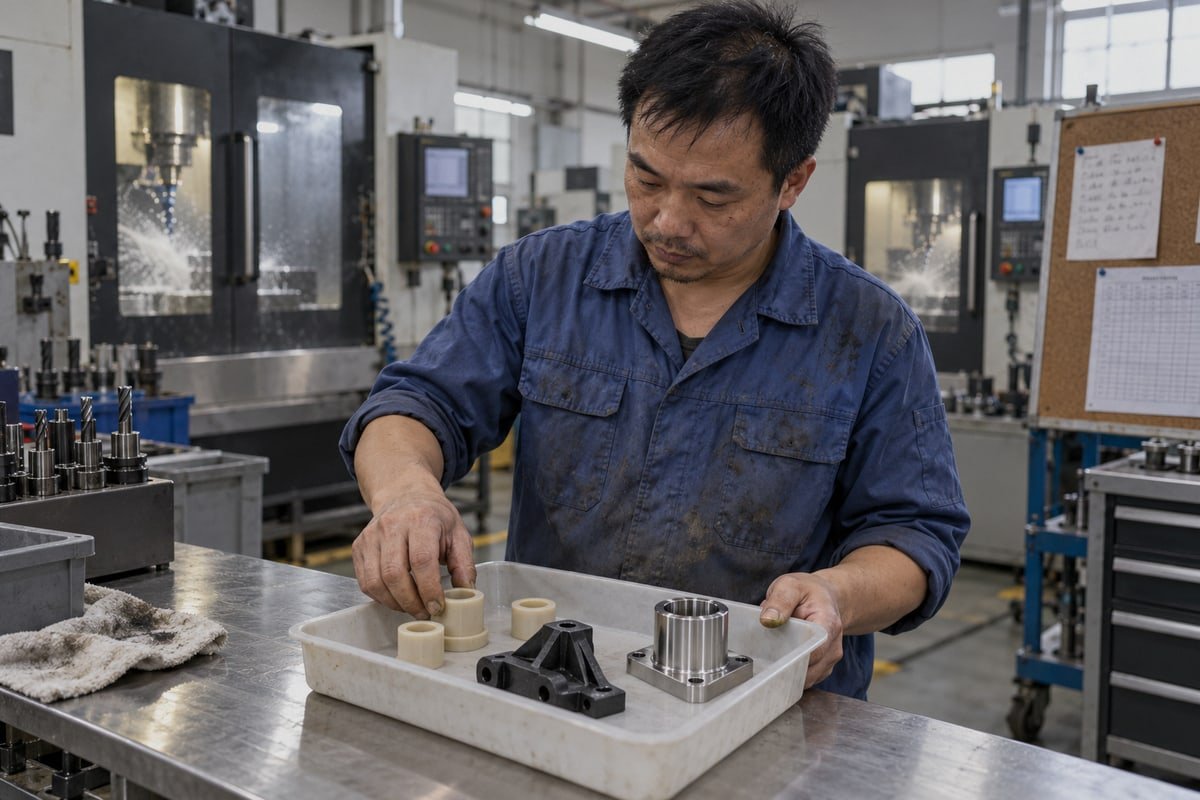
Picking a PEEK CNC machining supplier on price alone often ends with warped parts and missed launches. On our production line, PEEK is routine, and that difference decides the outcome.
Choose a PEEK CNC machining supplier that proves repeatable control of your exact PEEK grade: verified PEEK part examples, documented stress relieving and annealing, thin-wall workholding, temperature-stabilized inspection, material traceability, itemized quotes, and a pilot build. Judge process evidence, not the lowest first-piece price.
Below, I walk through the four questions buyers ask us most. Each one ends with something you can paste straight into your RFQ.
How can I verify a supplier's real experience machining PEEK material?
A German procurement manager once asked me to name the PEEK grades we ran that month. That question did more than any brochure could.
Verify real PEEK experience by asking which exact grades the supplier machines regularly—unfilled, GF30, CF30, or bearing grade—requesting anonymized examples of comparable parts, and asking how they handle heat, residual stress, and tooling. Vague answers about engineering plastics are a warning sign.

PEEK sits at the top of the high-performance thermoplastics 1 family. It resists heat, wear, and aggressive chemicals. That is why engineers specify it for pump seals, semiconductor fixtures 2, and medical housings. That same toughness makes it expensive. In our factory the material price still makes buyers pause. But PEEK itself is no longer exotic on our CNC milling and turning lines. We run it every week. That frequency is the first thing you should test in any supplier.
Ask about grades, not the material name
"PEEK" on a quote tells you almost nothing. Unfilled, glass-filled, carbon-filled, and bearing grades cut differently. Reinforced grades are abrasive. They dull standard carbide fast. A supplier who has actually run them will mention PCD or high-positive-rake carbide tooling without being prompted.
| PEEK grade | What it offers | What it demands from the supplier |
|---|---|---|
| Unfilled PEEK | Best chemical resistance, medical and food-contact options | Heat control to avoid smearing; very sharp tools |
| GF30 (30% glass fiber) | Higher stiffness, better dimensional stability | Abrasion-resistant tooling; frequent tool checks |
| CF30 (30% carbon fiber) | Highest stiffness, low wear, static dissipation | PCD tooling; dust control; strict tool-life limits |
| Bearing grade (PTFE/graphite filled) | Low friction, long wear life | Gentle clamping; care with surface finish |
Five questions that expose real experience
- Which PEEK grades did you machine in the last 90 days?
- Who supplies your stock—Victrex, Solvay, or a generic source—and can you show the certificate?
- Can you share anonymized photos of parts with similar walls, threads, or sealing faces?
- What defects have you seen on PEEK, and what did you change afterward?
- How do you decide when a tool is worn out on CF30?
A good answer is specific. A bad answer is "we machine all engineering plastics."
Specialist or general shop?
Buyers often ask me whether they need a PEEK-only specialist. I don't think so. We are a general precision shop in Dongguan. We machine aluminum, titanium, and PEEK on the same floor. What matters is evidence. If a general shop can show you its PEEK scrap bin, its tool-change log, and a finished part that passed CMM, it is qualified. If a "specialist" can only show a web page, it is not.
What tolerances and surface finish quality should I expect for PEEK CNC parts?
Every quote I review for PEEK forces one trade-off: tighter tolerances raise cost and lower yield, yet a sealing face cannot be loosened. We weigh this before pricing.
Expect a capable PEEK CNC machining supplier to hold general tolerances near ±0.05 mm, with critical features reaching ±0.01 mm when geometry, annealing, and temperature-stabilized inspection allow. Surface finishes of Ra 1.6 µm are standard; Ra 0.8 µm is achievable but should be specified only where function demands.
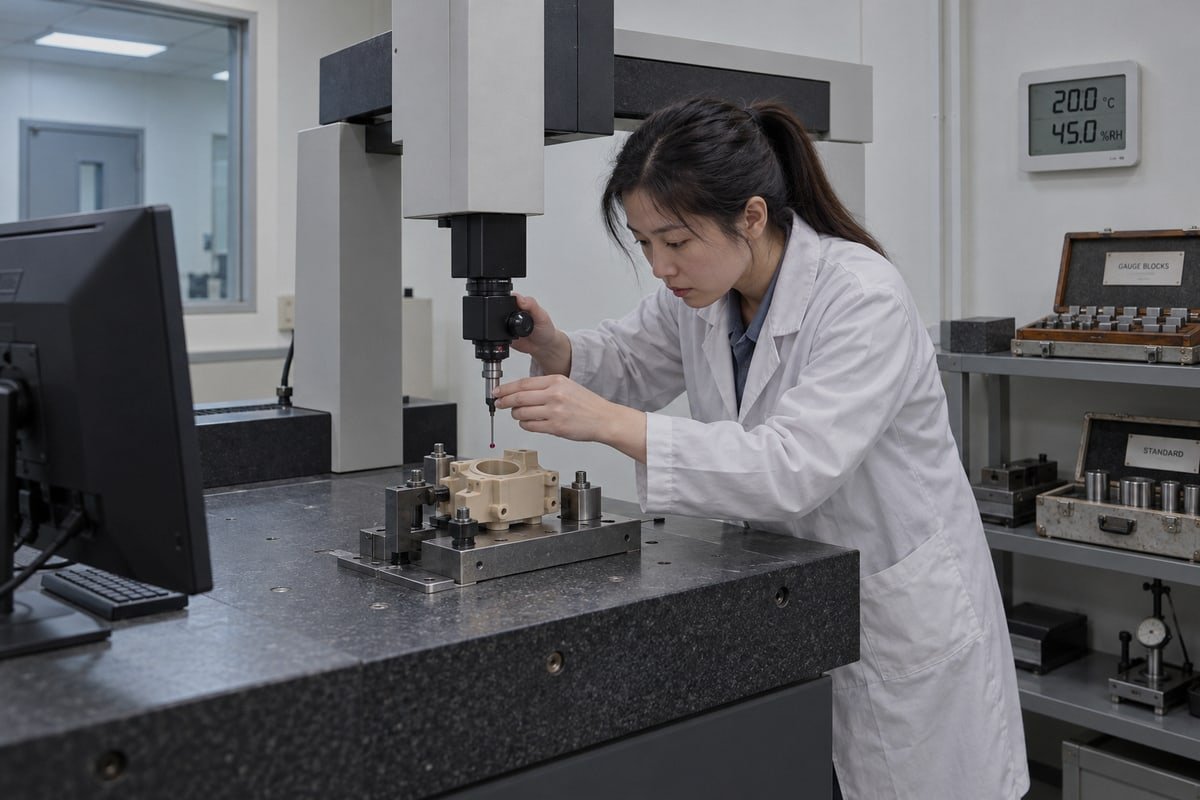
Tolerance talk with PEEK starts with physics, not promises. PEEK is semicrystalline. It carries residual stress from extrusion, and cutting releases that stress. Heat from the tool adds more. The part can "walk" by a few hundredths after it leaves the fixture, and again if it warms up near a window. Any supplier promising every tolerance without discussing this is guessing.
What controls dimensional stability
Three things decide whether a PEEK part holds size:
- Stress relieving and annealing before roughing, and often again between roughing and finishing.
- Workholding that supports thin walls without crushing them.
- Inspection after the part has rested at a controlled temperature, normally 20°C.
Our standard sequence on tight-tolerance PEEK 3 is rough, stabilize, finish, rest, measure. We treat the 20°C soak as part of the measurement method, not an extra service. Measuring a warm part straight off the spindle produces a nice report and a bad delivery.
Realistic tolerance expectations
| Feature type | What we quote with confidence | Main risk driver |
|---|---|---|
| General milled dimensions | ±0.05 mm | Thermal growth during cutting |
| Bores and bearing fits | ±0.01 to ±0.02 mm | Stress release after unclamping |
| Flatness on thin plates | Tighter than 0.05 mm needs intermediate annealing | Residual stress, clamping distortion |
| Threads | Standard 6H/6g classes | Tool dwell, melting in the root |
| Critical positional features | ±0.01 mm with a 5-axis single setup | Tolerance stacking across setups |
Our 3-axis, 4-axis, and 5-axis mills reach 0.01–0.005 mm on metals. On PEEK, we only promise the tight end after the DFM review confirms the geometry can be supported and stabilized.
Surface finish on PEEK
Unfilled PEEK finishes well. Ra 1.6 µm is the normal milled result. Ra 0.8 µm is reachable with sharp finishing passes and light engagement. Carbon-filled grades look matte and slightly grainy because fibers sit at the surface. That is normal, not a defect. If your drawing calls for a mirror finish on CF30, your supplier should push back.
Should you accept looser tolerances?
Here is the trade-off I raise in every DFM review. Tight tolerances everywhere raise price and reduce yield. But I will never suggest loosening a seal groove, a valve seat, or a press-fit bore. Relax the cosmetic faces. Keep the functional ones. Some vendors now advertise digital-twin thermal simulation. Ask them something simpler: what did the first article measure after 24 hours at 20°C?
How do I avoid unstable batch production quality when outsourcing PEEK machining?
Last spring our inspection room flagged a batch of CF30 PEEK bushings. Bore sizes drifted after the fourth tool change. We caught it because we check after stabilization.
Avoid unstable batch quality by locking the machining sequence after the pilot build, requiring tool-life limits, consistent annealing, fixed workholding, lot-level material traceability, agreed inspection frequency, and formal change control. Run a small pilot lot first, then freeze the process before releasing recurring production.
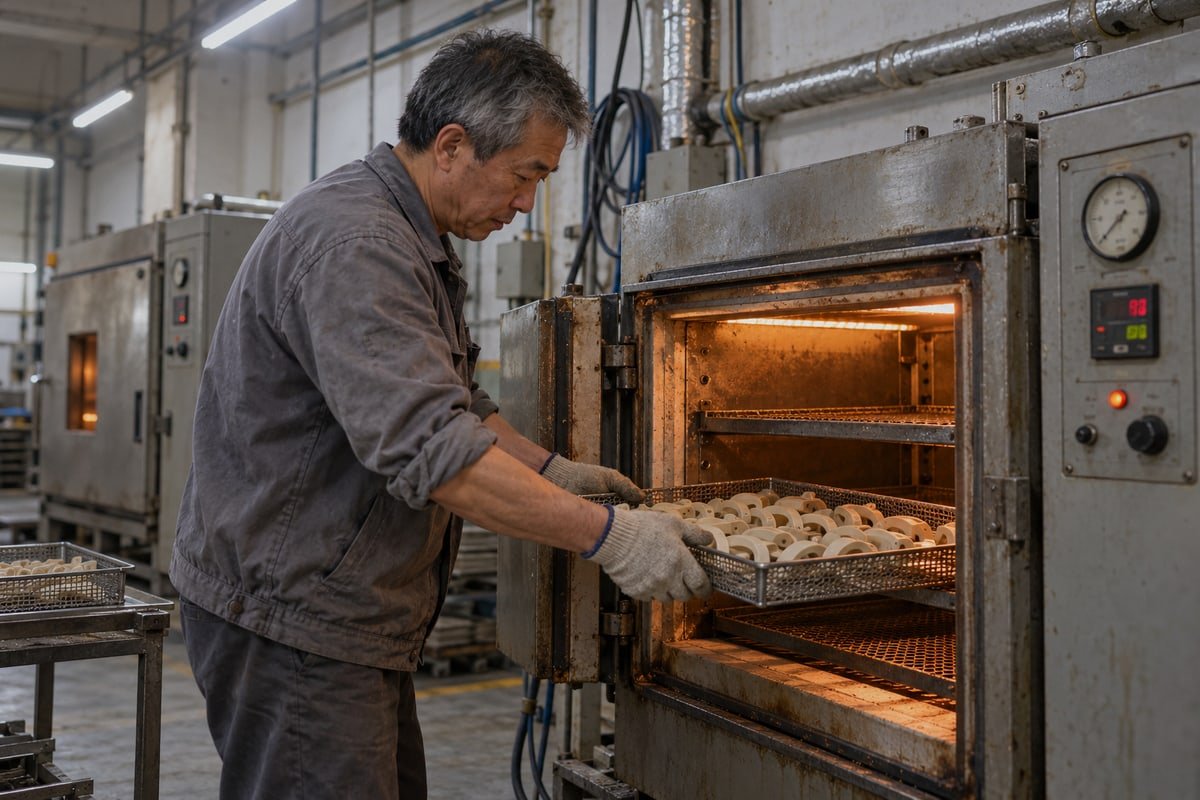
Samples pass. Batches drift. This is the most common complaint I hear from buyers who left a previous PEEK CNC machining supplier. The sample was made slowly, by the best operator, with a fresh tool. Production was made fast, by whoever was free, with a tool that was "still fine." PEEK punishes that gap harder than aluminum does.
Why PEEK batches drift
- Tool wear: glass and carbon fibers dull edges quickly, so the tenth part sees more heat and rubbing than the first.
- Stock lot variation: different extrusion lots carry different residual stress.
- Clamping force: a new operator tightens the vise harder, and the thin wall springs back differently.
- Heat buildup: continuous cycles warm the fixture and the part.
- Skipped annealing: someone drops the intermediate stress relief to save a day.
A workflow that freezes the process
- Define the application: temperature, chemical exposure, load, cleanliness, and failure consequence.
- Lock the material: exact grade, resin manufacturer, stock form, color, and allowed equivalents in writing.
- Send a complete RFQ: 3D model, 2D drawing, GD&T, quantity, annual demand, inspection and packaging needs.
- Compare itemized quotes covering material, setups, annealing, inspection, documentation, packaging, and freight.
- Run a pilot lot with first-article inspection, and measure it again after stabilization.
- Freeze the sequence: tool-life limits, fixture, program, annealing schedule, and inspection frequency.
- Agree change control: no material substitution or process change without written notice.
- Qualify a second source only after the first process is stable.
Prototype supplier vs production supplier
| Priority | Prototype stage | Recurring production |
|---|---|---|
| Minimum order | One piece, no MOQ | Stable monthly lots |
| Lead time | As short as 5 days in our shop | Predictable schedule, backup capacity |
| Documentation | Basic dimensional report | FAI, lot traceability, process records |
| Tooling | Fresh tool per job | Logged tool-life limits |
| Change handling | Fast revisions | Formal change notification |
Volume changes the math in another way. Once quantities climb into the thousands, injection molding 4 may beat machining after tooling is amortized. Below that, machining avoids tooling cost and keeps design changes cheap. Compare total landed cost, not the machining line alone.
Local versus overseas, the honest version
A buyer in Ohio asked me why he should ship PEEK parts from China when a local shop quoted noticeably more. My answer was: compare the cost of a nonconformance, not the hourly rate. If we miss, the fix takes a flight. So we inspect at origin, send CMM data before shipping, and pack each part separately. If a supplier, local or overseas, cannot show you that, the price gap is not real savings. Also ask about scrap handling. PEEK swarf has value, and a shop that tracks it usually tracks everything else too.
What documents and certifications should I request from my PEEK CNC machining supplier?
I learned early that a certificate hanging on a wall says little about PEEK. Our ISO 9001:2015 system matters only because it forces records you can actually audit.
Request a material certificate with resin manufacturer and lot number, a certificate of conformance, first-article inspection report, dimensional inspection or CMM report, surface-finish results, calibration records, annealing process record, and the supplier's ISO 9001 certificate. Add ISO 13485 or AS9100 requirements where your industry demands them.
Paperwork is where price gaps often hide. A cheap PEEK quote frequently excludes the material certificate, the inspection report, and the annealing step. By the time you ask for them, the price climbs. So I tell buyers to list the documents in the RFQ, before the quote, not after.
The document set for PEEK parts
| Document | What it proves | When to require it |
|---|---|---|
| Material certificate (resin maker, grade, lot) | Material traceability; no generic substitution | Always |
| Certificate of conformance | Parts meet drawing and purchase order | Always |
| First-article inspection report | The process produces the drawing | Pilot lot and after any change |
| CMM or dimensional report | Critical features measured, with conditions stated | Tight-tolerance parts |
| Surface-finish results | Ra meets drawing | Sealing and bearing faces |
| Annealing / process record | Stress relief actually happened | Thin walls, flat parts, seals |
| Calibration records | Measuring tools are trustworthy | On audit request |
| Nonconformance procedure | How problems get fixed | Recurring production |
What certifications prove, and what they don't
ISO 9001:2015 certification, which our factory holds, proves that document control 5, calibration, traceability, and corrective action exist as systems. It does not prove PEEK competence. ISO 13485 certification matters when you build medical devices, especially when you use medical grade PEEK for implant or patient-contact parts. AS9100 certification matters for aerospace programs. If your project needs those, state it in the RFQ and verify the certificate number. Don't accept a logo. For high-vacuum or implant work, also ask whether the shop offers controlled-environment machining or cleanroom packaging to limit hydrocarbon and particle contamination. Our 30-day warranty covers what leaves our door, but good documents are what let your own quality team accept the parts without a second round of questions.
Red flags in the paperwork
- The supplier cannot name the exact grade or resin manufacturer on the certificate.
- The inspection report lists no temperature or stabilization time.
- "Annealed" appears on the quote, but no process record exists.
- A material substitution is proposed by email with no formal approval step.
- The quote lists inspection, certificates, or packaging as "optional."
Pre-award checklist
Exact grade confirmed. Material certificate available. Comparable PEEK parts verified. Rough-stabilize-finish strategy explained. Thin-wall workholding addressed. Inspection conditions defined. First-article report agreed. Quote fully itemized. Pilot build completed. Change control documented. Tick all ten, and the hourly rate becomes a secondary number.
Conclusion
Cheap PEEK quotes hide rework, delays, and warped parts. Qualify your PEEK CNC machining supplier on grade experience, annealing, inspection, and documents, then run a pilot build.
Footnotes
1. Scientific overview of high-performance polymers and their engineering properties. ↩︎
2. Global industry standards for semiconductor manufacturing equipment and materials. ↩︎
3. Scientific discussion of residual stress and its impact on achieving tight tolerances in polymers. ↩︎
4. Comprehensive overview of the injection molding process as an alternative to CNC machining. ↩︎
5. International standards for document control within a quality management system. ↩︎

 English
 Italiano
 Français
 日本語
 Deutsch (Sie)
 Español
 Русский
 العربية
 Български
 Čeština
 Dansk
 Suomi
 עִבְרִית
 हिन्दी
 Nederlands
 Português
 Română
 Slovenčina
 Svenska
 ไทย
 Tiếng Việt
 Türkçe
 Slovenščina