
A [CNC machining cost breakdown](https://stcncmachining.com/?p=15397) confuses many buyers who send us drawings in Dongguan. Three quotes, three prices, no explanation. That uncertainty stalls projects. I want to fix that here.
A CNC machining cost breakdown combines material, programming, setup, machine time, tooling, inspection, finishing, scrap allowance, and overhead. Fixed costs like setup are divided by quantity; variable costs like cutting time repeat per part. The final quote reflects total process cost, not one hourly rate.
The biggest pain point I hear from procurement managers is simple. Quotes from different suppliers vary wildly, and nobody can tell which number is fair. The sections below walk through each cost block, one at a time, so you can read any quote and judge it yourself.
How do material choices affect my CNC machining cost?
One stainless 316 housing on our Dongguan line chewed through several end mills before the first article passed. The material cost was modest. The tooling and time were not.
Material choices affect CNC machining cost twice. First, you pay for the full stock block, bar, or plate, including chips. Second, harder or gummier alloys cut slower and wear tools faster, raising cycle time and tooling costs. Material usually represents 10–50% of part price.
Why you pay for the billet, not the part
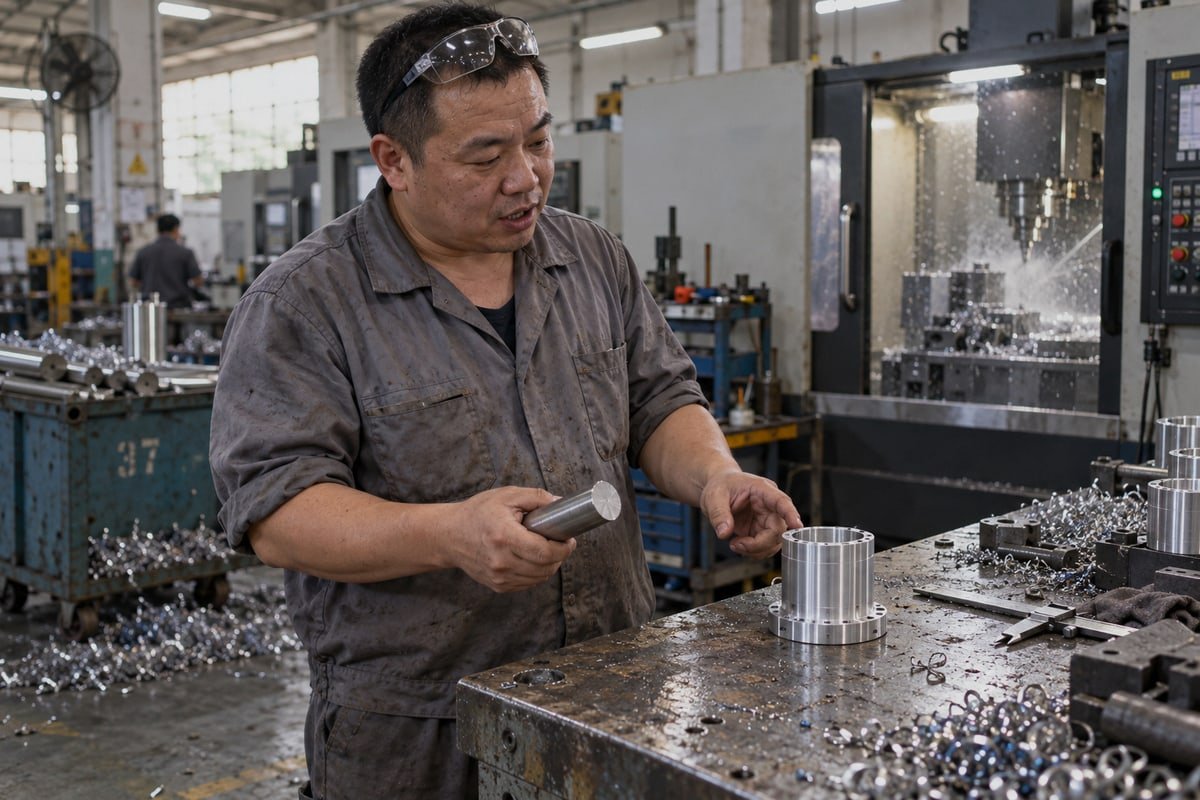
A quote is built on the stock we must buy, not the volume of the finished part. If your part is a thin cylindrical housing 1 with a flared base, we still start from a solid round bar or block large enough to hold the flange. Most of that bar becomes chips. Machinists call this the buy-to-fly ratio. A small finished part can carry a large material bill when it must be carved from a big block. That is why part weight alone is a poor predictor of price.
Other material cost drivers matter too. Standard stock sizes are cheaper than odd sizes. Minimum purchase quantities can force us to buy more than a single prototype needs. Material certificates 2 and traceability add paperwork and sometimes a premium on the raw bar. Heat-treated or pre-hardened stock costs more up front but may save a later process step. On larger batches, we can sometimes offset part of the bill through scrap recovery credits on aluminum or copper chips, but this only moves the needle at real production volume.
Machinability ratings and the second cost hit
Material selection also changes cutting speed, tool life, and risk. Machinability ratings give a rough guide. Free-cutting aluminum sits near the top. Austenitic stainless runs slower and work-hardens. Titanium and nickel alloys demand low speeds, rigid fixturing, and frequent tool checks. Engineering plastics such as PEEK or POM cut quickly but need careful clamping to avoid deflection.
| Material group | Relative stock cost | Machinability | Tooling and time impact |
|---|---|---|---|
| 6061 / 7075 aluminum | Low to medium | Excellent | Fast cycle times; cosmetic grades cost more |
| Brass / copper | Medium | Very good | Fast cutting; copper can be gummy |
| 304 / 316 stainless | Medium | Fair | Slower feeds, more tool wear, more heat |
| Alloy and tool steel | Medium to high | Fair to poor | Rigid setups, hardened grades need special tooling |
| Titanium / nickel alloys | High | Poor | Long cycles, high tooling costs, higher scrap risk |
| PEEK / POM / nylon | Medium (PEEK high) | Good | Fast cutting; stability and deflection control needed |
Published breakdowns put material at roughly 10–30% of part price in one estimate and 30–50% in another. Both are honest. The spread simply shows how much the mix changes from job to job. A titanium medical bracket is material-heavy. An aluminum automation plate is time-heavy. When I review a drawing, I always ask whether the alloy was chosen for function or by habit, because swapping 316 for 304 or 7075 for 6061 can be the single cheapest change on the sheet.
What role does part complexity play in my machining quote?
Every week I weigh the same question: run a bracket on a 3-axis mill with six setups, or on a 5-axis center with two. The cheaper hourly rate rarely wins.
Part complexity drives three cost blocks: programming hours, setup count, and cycle time. Deep pockets, thin walls, small internal radii, and tight tolerances slow cutting and add inspection. A visually simple part with one difficult feature can cost more than an intricate part designed for multi-axis machining.
Visual complexity versus manufacturing complexity
Buyers often judge complexity by how a part looks. Machinists judge it by how it must be held and cut. A flat plate with one deep, narrow pocket and a 0.01 mm tolerance can cost more than a sculpted impeller programmed for simultaneous 5-axis work. Geometric complexity raises cost through specific features: deep pockets that need long-reach tools, small internal radii that force small cutters, thin walls that chatter, undercuts that need special tooling, and holes at odd angles that demand extra orientations.
Setup and programming are fixed charges
Before the spindle turns, our engineers read the CAD and drawing, pick tools, plan workholding, generate toolpaths, and simulate for collisions. Industry guides put programming for simple jobs at about $100–$500 per project, and simple setups at $50–$150 versus $500 to more than $1,000 for complex multi-operation work. These are illustrative ranges, not fixed prices. The key point is that setup and programming are mostly fixed per job. A $300 programming fee is painful on one prototype and nearly invisible across a thousand parts.
Machine hourly rate and why 5-axis can be cheaper
The machine hourly rate recovers equipment depreciation 3, maintenance, tooling-driven spindle wear, coolant, electricity, software, labor, and margin. Some shops now index part of that rate to real-time energy prices on long, high-consumption runs. One common set of ranges looks like this:
| Machine class | Indicative hourly rate | Typical strength | Cost caveat |
|---|---|---|---|
| 3-axis milling | $30–$60 | Prismatic parts, plates, simple housings | More setups for multi-face parts |
| 4-axis milling | $50–$100 | Rotational features, indexed faces | Better than 3-axis for round housings |
| 5-axis milling | $75–$150 or more | Complex surfaces, fewer setups | Higher rate, higher programming skill |
Here is the objection I hear most: "Your 5-axis rate is double, so the part must cost double." It does not. If a housing needs six orientations on a 3-axis machine and two on a 5-axis machine, the 5-axis route saves four setups, four alignment risks, and hours of handling. Total process cost equals rate times billable time plus setup, tooling, inspection, and risk. The cheapest hourly rate is not the cheapest part.
Tight tolerances add another layer. Holding 0.01–0.005 mm means slower finishing passes, temperature awareness, probing, and often CMM measurement. Our factory runs these jobs daily, but we quote them honestly because the time is real. The best drawings put tight tolerances only on fit-critical features and leave the rest at general tolerance.
How can I reduce my CNC machining costs without sacrificing quality?
A procurement manager in Germany forwarded me three quotes for the same optical mount. The prices differed widely. He asked which one was honest. The answer sat in the scope.
Reduce CNC machining costs by relaxing noncritical tolerances, enlarging internal radii, limiting pocket depth, designing for fewer setups, choosing standard stock sizes, and ordering realistic batch quantities. Request DFM feedback before programming starts, and compare quotes on identical scope so you cut cost, not quality.

Start with a worked CNC machining cost breakdown
Numbers make this concrete. Below is an illustrative quote for one aluminum prototype, not an industry average.
| Cost block | Single prototype | Ten parts (per unit) |
|---|---|---|
| Materiaal | $35.00 | $35.00 |
| Programming and process planning | $180.00 | $18.00 |
| Setup and workholding | $220.00 | $22.00 |
| Machining (2.5 h × $75/h) | $187.50 | $187.50 |
| Tooling and consumables | $25.00 | $25.00 |
| Inspection | $60.00 | $60.00 |
| Deburring and anodizing | $90.00 | $90.00 |
| Packaging and shipping | $35.00 | $35.00 |
| Risk and rework allowance | $40.00 | $40.00 |
| Total per part | $872.50 | $512.50 |
The $400 of setup and programming does not change. It is simply spread over ten parts. That is the entire logic of production volume. A simpler version: $600 fixed plus $140 variable gives $740 at one part, $200 at ten, and $146 at a hundred.
Where the real savings sit
Design changes give the biggest wins because they shrink variable cost on every part:
- Relax noncritical tolerances and apply tight ones only to functional interfaces.
- Increase internal radii so we can use larger, faster cutters.
- Reduce pocket depth and keep walls as thick as function allows.
- Align holes with one or two tool directions to cut setups.
- Use standard hole sizes, threads, and stock dimensions.
- Limit cosmetic surfaces to faces people actually see.
Process changes help next. Reusing proven programs, batching identical parts, and using standard vises instead of custom fixtures all reduce setup and programming load. We often return a DFM note within the quote stage because one radius change can remove an hour of cycle time.
Two objections buyers raise
First: "More parts always means a lower unit price." Not always. A large order can require dedicated fixtures, pallet systems, extra inspection capacity, and material commitments. Unit cost falls, but total project cost and inventory risk rise. Order what your schedule truly needs.
Second: "The lowest quote is the best deal." That German buyer's cheapest quote excluded inspection reports, material certificates, and anodizing. The highest one included all of them plus freight. Once I aligned the scope, the spread shrank dramatically. Ask every supplier the same questions: Is programming included? How many setups are assumed? Is finishing priced separately? Are certs, reports, shipping, and taxes included? Is this the price of an accepted part or only machining time? Our 20 years of exporting to Europe and North America taught us that a clear, line-item quote prevents the surprise price increases buyers fear most.
Why do surface finishing and inspection add to my final price?
Years ago we learned a hard lesson on anodized camera housings: two batches, two slightly different shades, one rejected shipment. Finishing is never a free final step.
Surface finishing and inspection add cost because they are separate processes with their own labor, equipment, lot minimums, and risk. Anodizing, plating, or polishing typically adds 5–20% of price; inspection and documentation add roughly 5–15%. Both turn a machined blank into an accepted, certified part.
What post-processing services actually involve
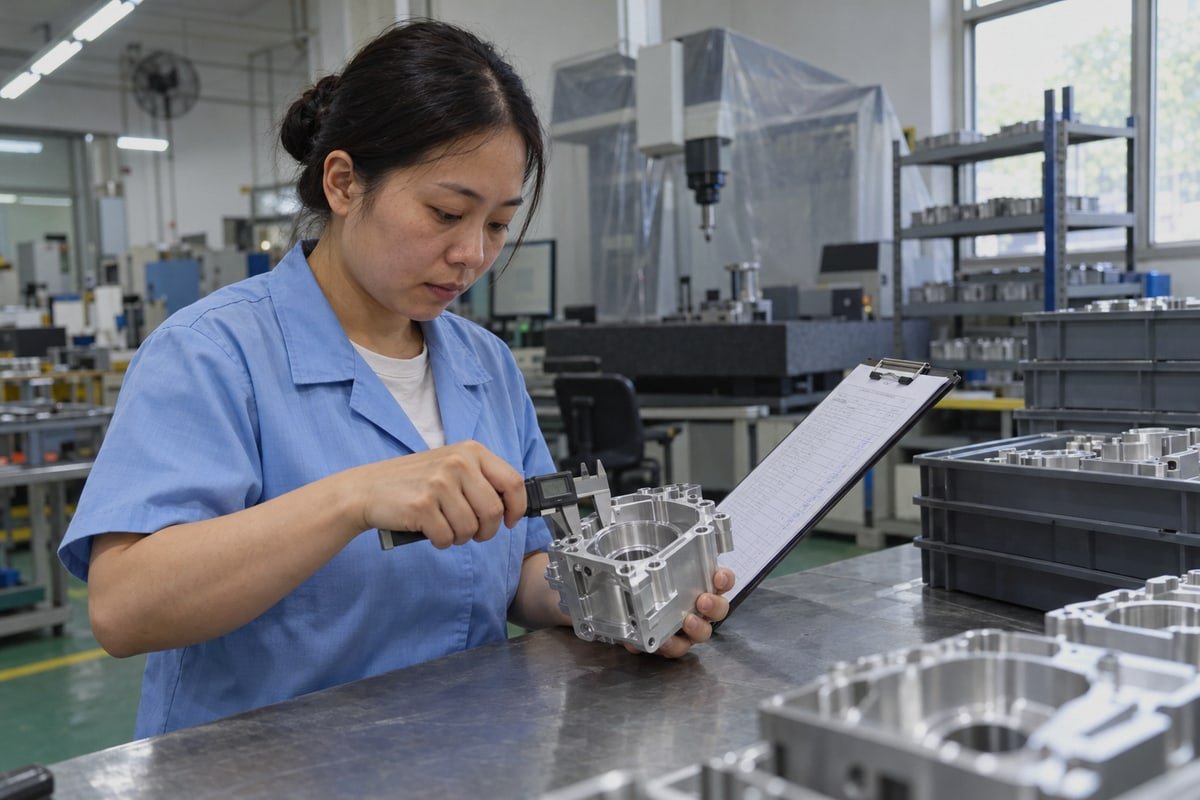
CNC machining produces the shape. Everything after that is secondary work. Deburring, tumbling, bead blasting, brushing, polishing, anodizing, plating, powder coating, passivation, heat treatment, black oxide, and laser marking each add handling and time. Some we run in-house. Others go to specialist partners, which adds transport, minimum lot charges, and schedule risk.
| Finishing process | Usually charged | Main cost drivers |
|---|---|---|
| Deburring / tumbling | Per part | Edge count, part size, cosmetic standard |
| Bead blasting | Per part or lot | Masking, uniformity, media type |
| Anodizing (Type II / III) | Per lot with minimum | Color consistency, masking, thickness spec |
| Plating / passivation | Per lot with minimum | Certification, racking, outsourced transport |
| Polishing | Per part | Target roughness, geometry, labor hours |
| Heat treatment | Per lot | Alloy, hardness spec, post-treatment re-machining |
Here is an objection worth resolving: "Finishing just inflates the price." Sometimes finishing lowers it. Reaching a mirror-like appearance through extra machining passes can cost more than a fast bead blast followed by anodizing. We distinguish a machined finish from a post-processed finish on every quote. The right choice depends on the surface roughness, color, and corrosion resistance you need.
Inspection buys acceptance, not just measurement
Inspection cost covers operator checks with micrometers, first-article inspection, CMM runs, in-process probing, material certificates, and written reports. Published breakdowns put inspection and documentation at about 5–15% of price, and aerospace or medical work can exceed that. The number rises with tight tolerances and GD&T callouts.
Under our ISO 9001:2015 4 system, we check specifications during production and inspect again before shipment, then back the parts with a 30-day warranty. That process is part of the quote. A cheaper competitor may skip the CMM report or the material cert. The part looks the same on screen but it is not the same product. Think of the price as the cost of acceptance. It includes prevention of scrap, rework allowance, and the documents your own quality team needs.
Logistics and the new surcharges
Finally, packaging and shipping belong in the breakdown. Precision parts need foam, separation, and sometimes vacuum sealing. Expedited lead times, which we can hold to as short as 5 days on suitable jobs, may require overtime and priority finishing. Across global sourcing, buyers now see supply chain resilience 5 surcharges replacing the old labor-only arbitrage. A quote that states freight terms, customs paperwork, and insurance openly is easier to trust than one that leaves them out.
Conclusion
Opaque quotes waste weeks and budgets. Understanding the CNC machining cost breakdown lets you compare scope, fix costly features early, and buy with confidence. Send drawings; we'll show the numbers.
Footnotes
1. Overview of machining processes used to produce cylindrical components from solid stock. ↩︎
2. NIST provides guidance on standards and documentation, including material certificates used for industrial traceability. ↩︎
3. Explains the accounting concept of depreciation used to calculate machine hourly rates in manufacturing. ↩︎
4. Official ISO page for the quality management standard mentioned in the article’s inspection section. ↩︎
5. Authoritative resource on the economic factors and surcharges affecting modern global supply chain resilience. ↩︎

 Nederlands
 English
 Italiano
 Français
 日本語
 Deutsch (Sie)
 Español
 Русский
 العربية
 Български
 Čeština
 Dansk
 Suomi
 עִבְרִית
 हिन्दी
 Português
 Română
 Slovenčina
 Svenska
 ไทย
 Tiếng Việt
 Türkçe
 Slovenščina